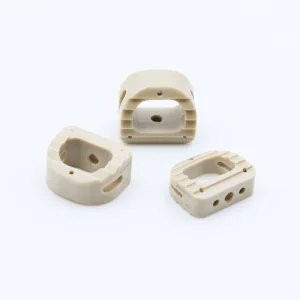
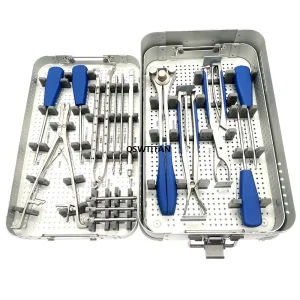
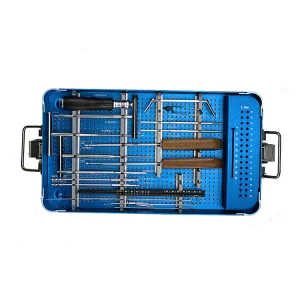
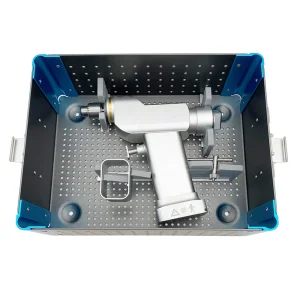
HBM Medical Apparatus And Instruments Co., Ltd. stands as a premier orthopedic medical equipment R&D, manufacturing, and operational enterprise in China. With an extensive sales network covering the whole country and operational offices across multiple key regions, HBM has established itself as an indisputable pillar in the global medical supply chain. Driven by rigorous international standards, cutting-edge production equipment, and visionary technical teams, our manufacturing ecosystem delivers unmatched reliability for medical professionals worldwide.
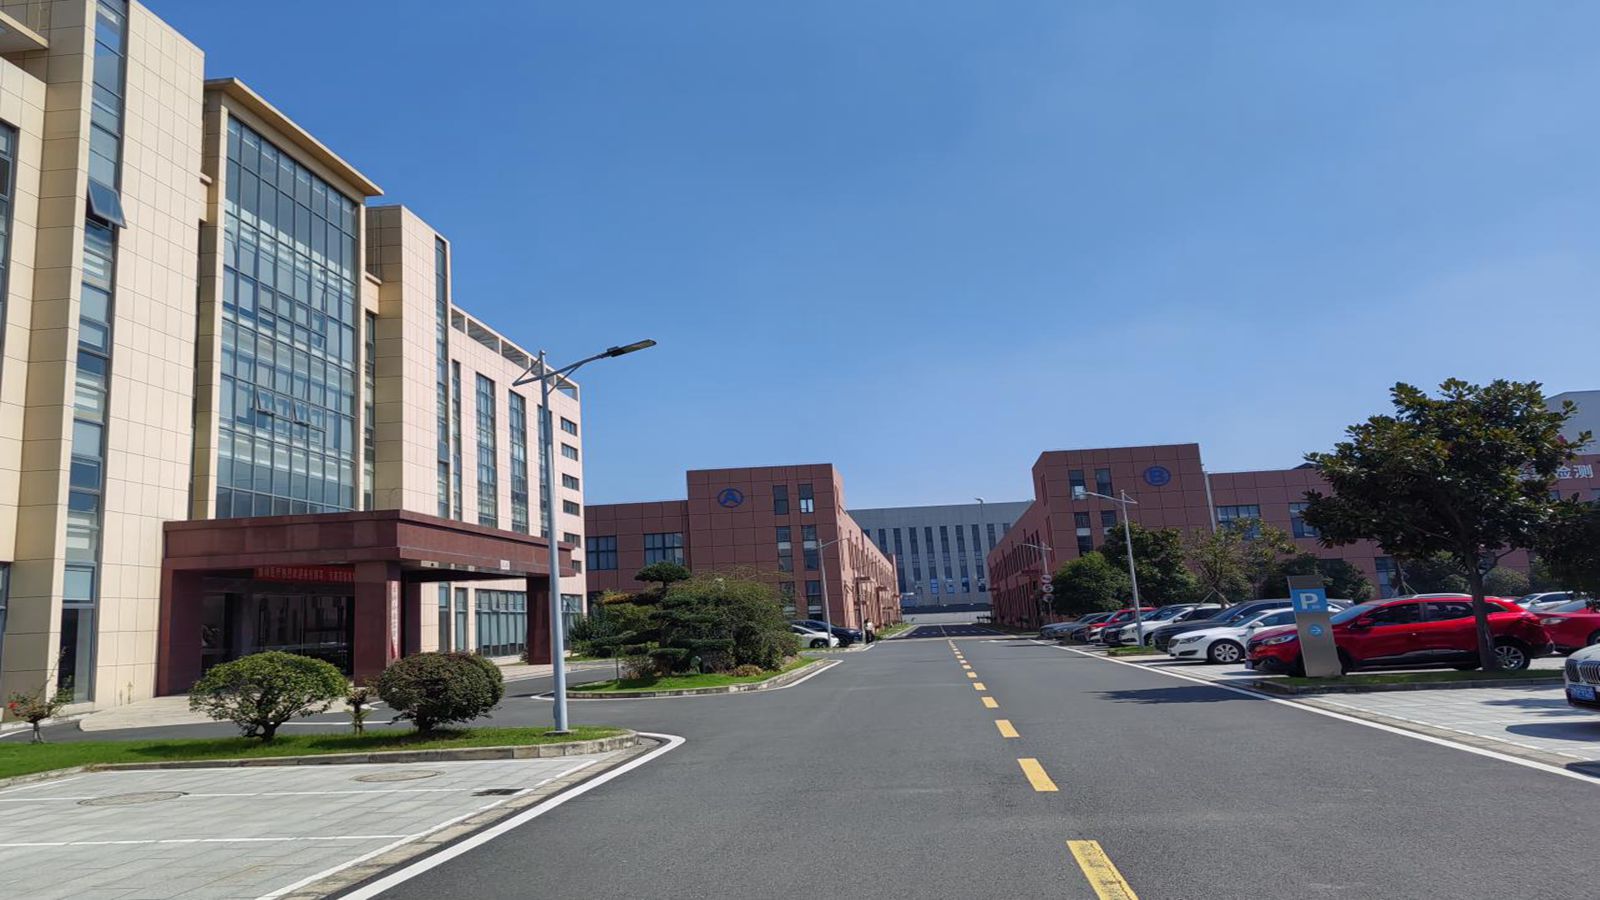
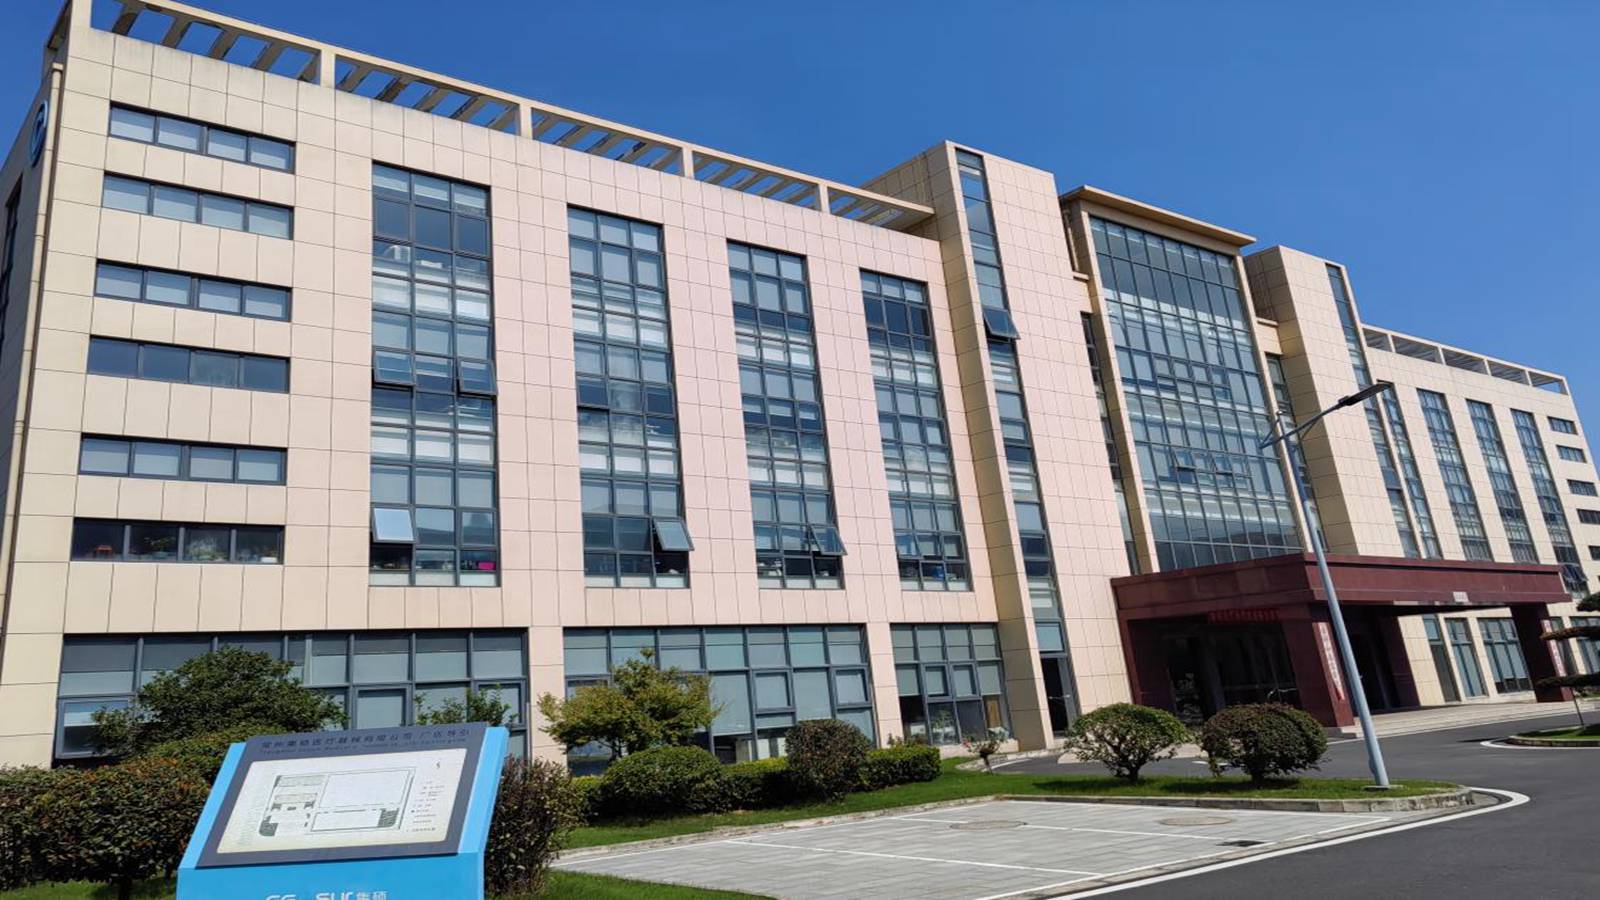
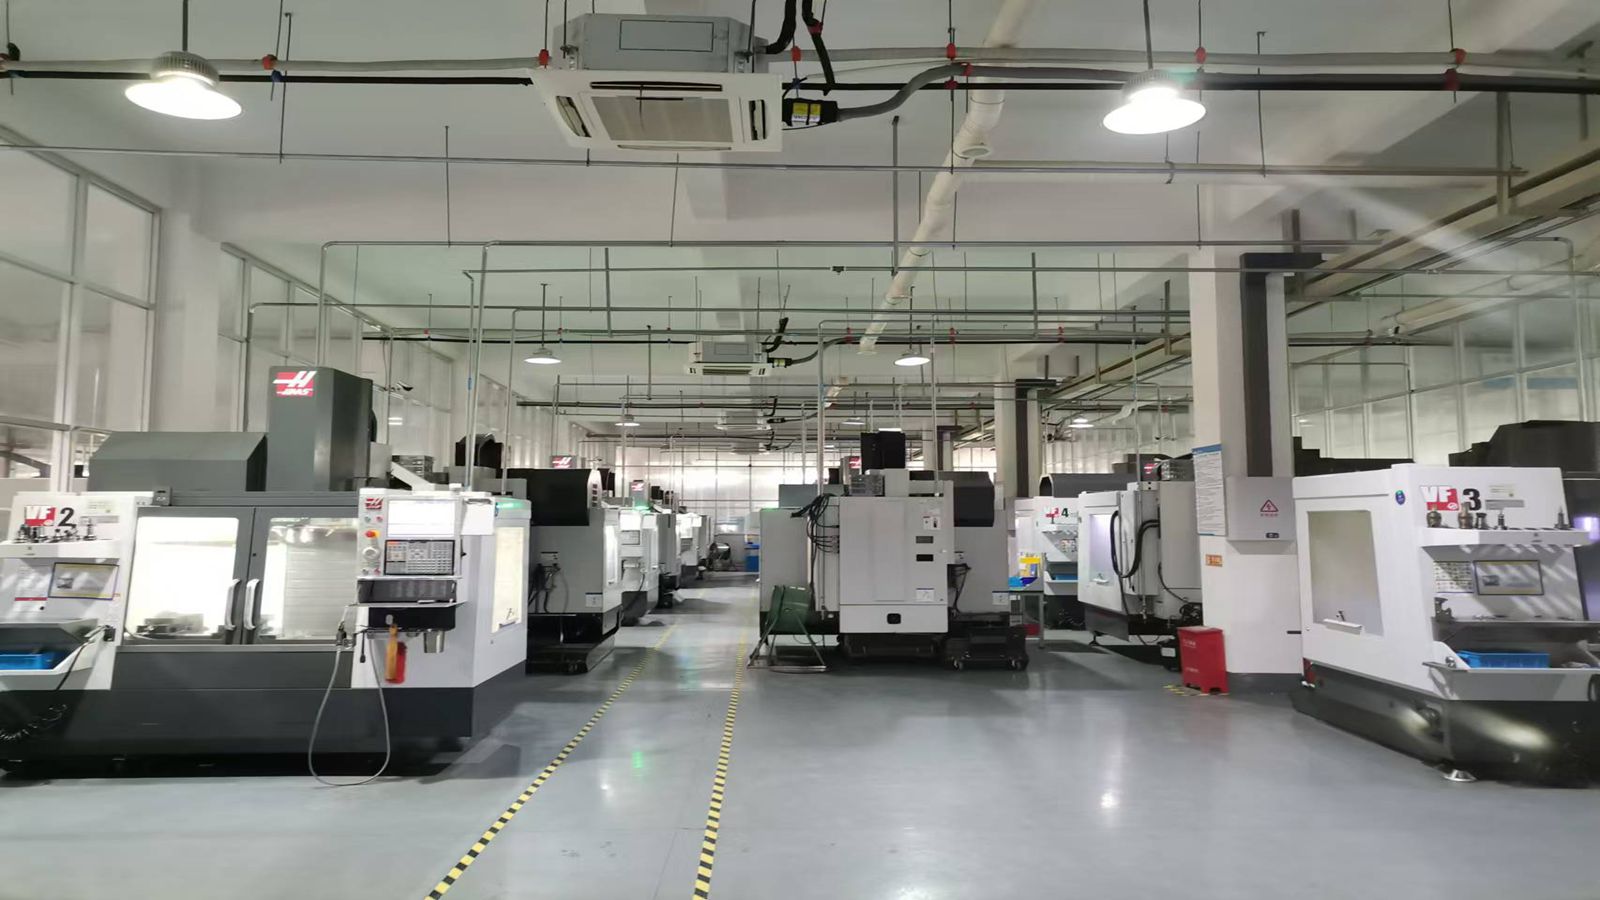
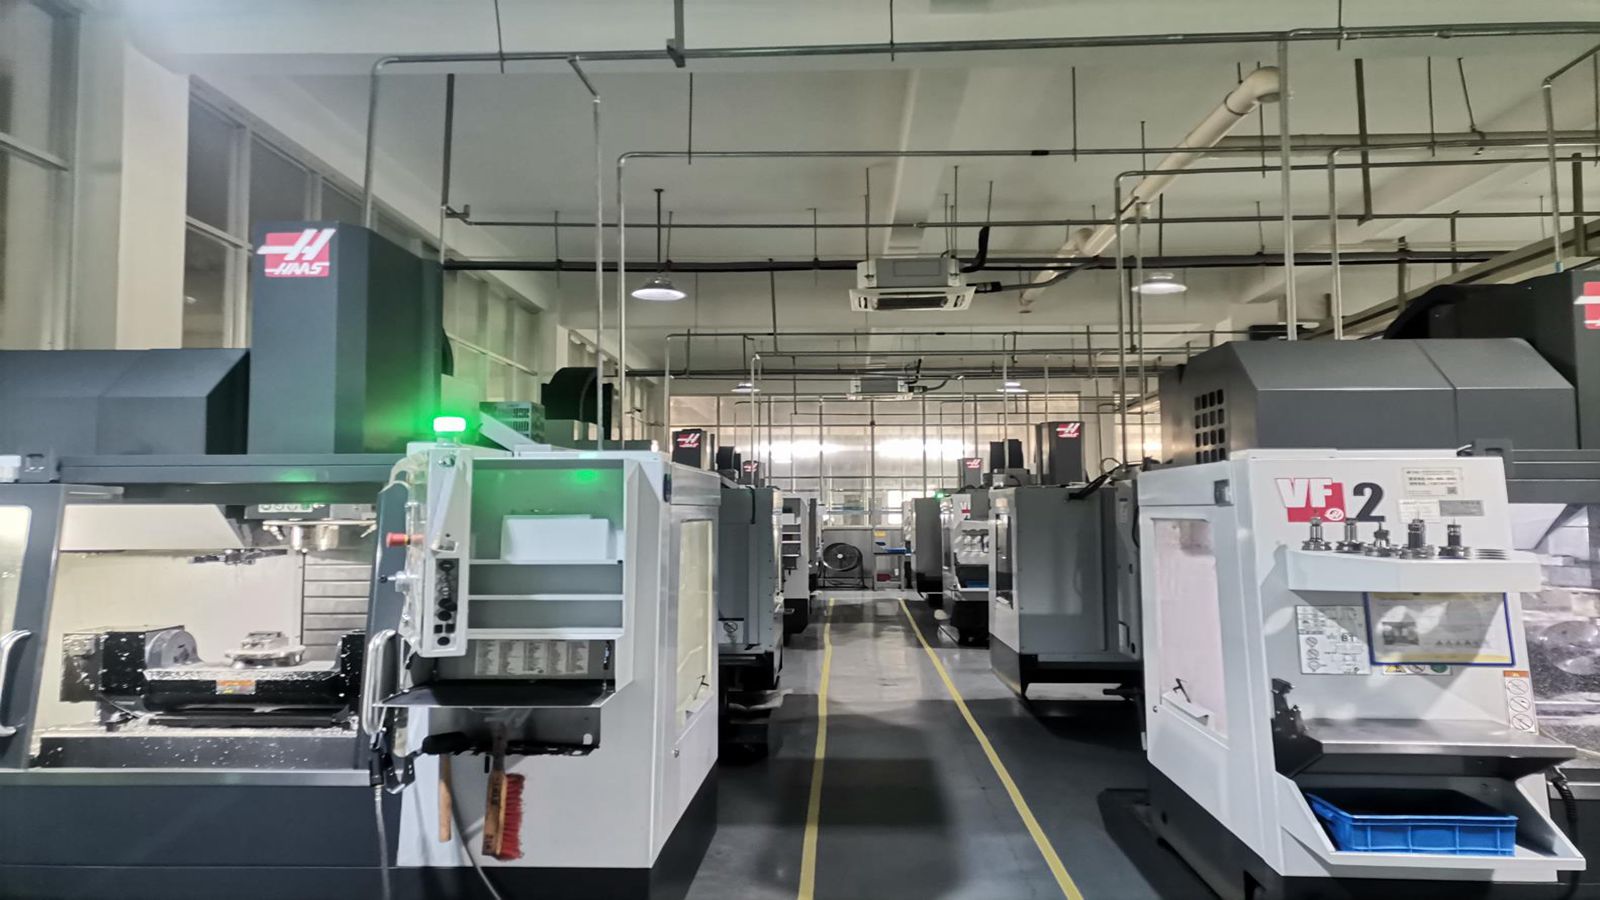
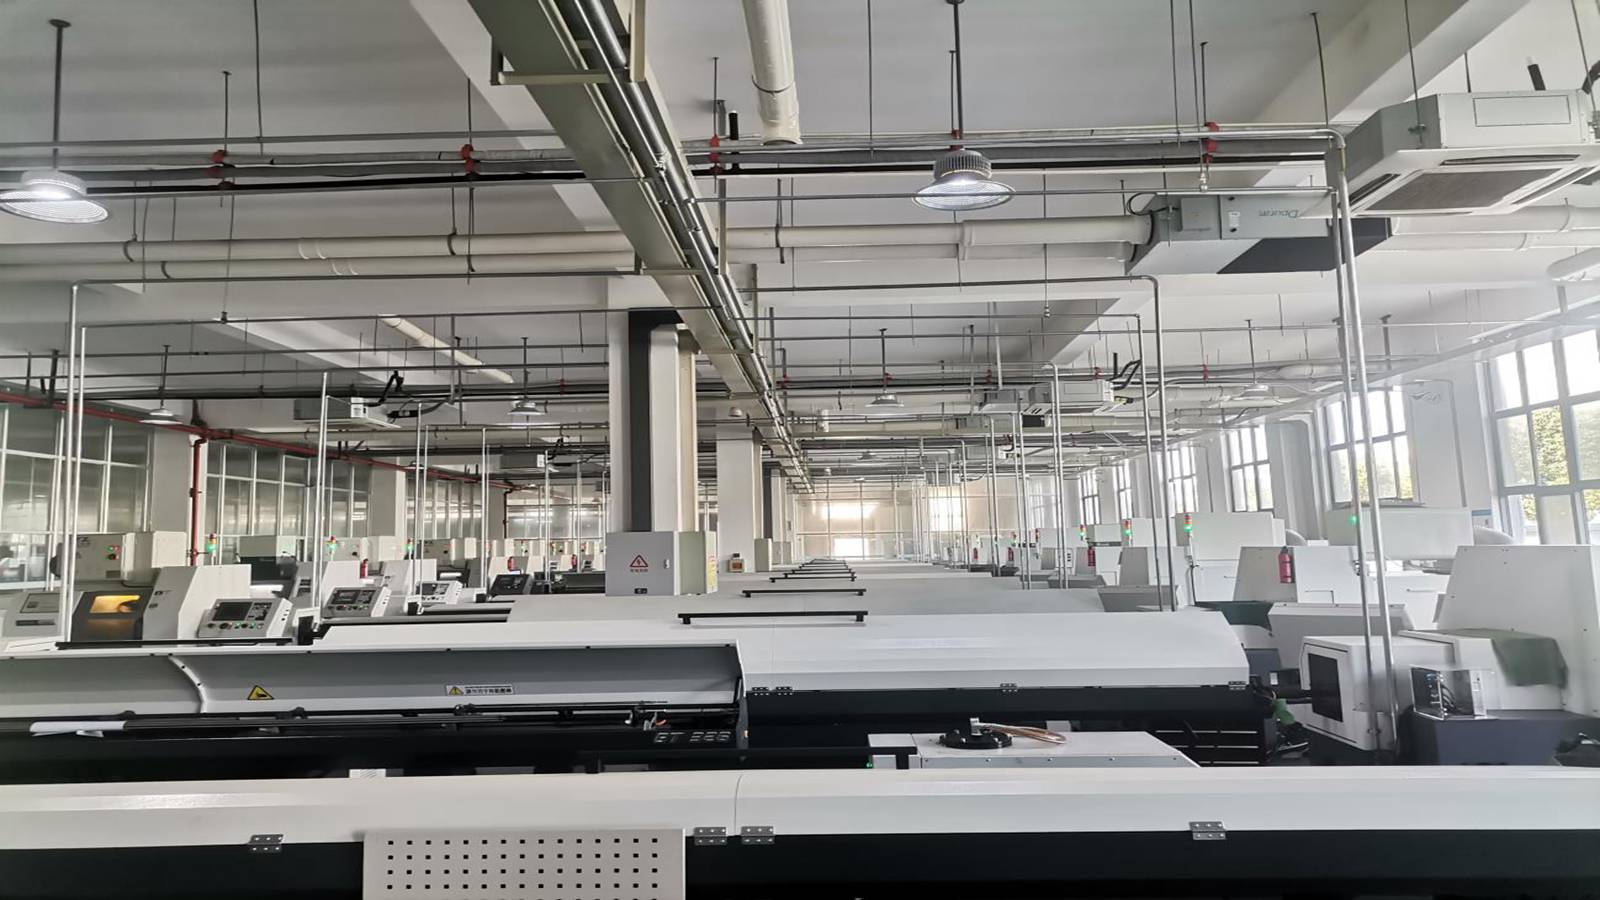
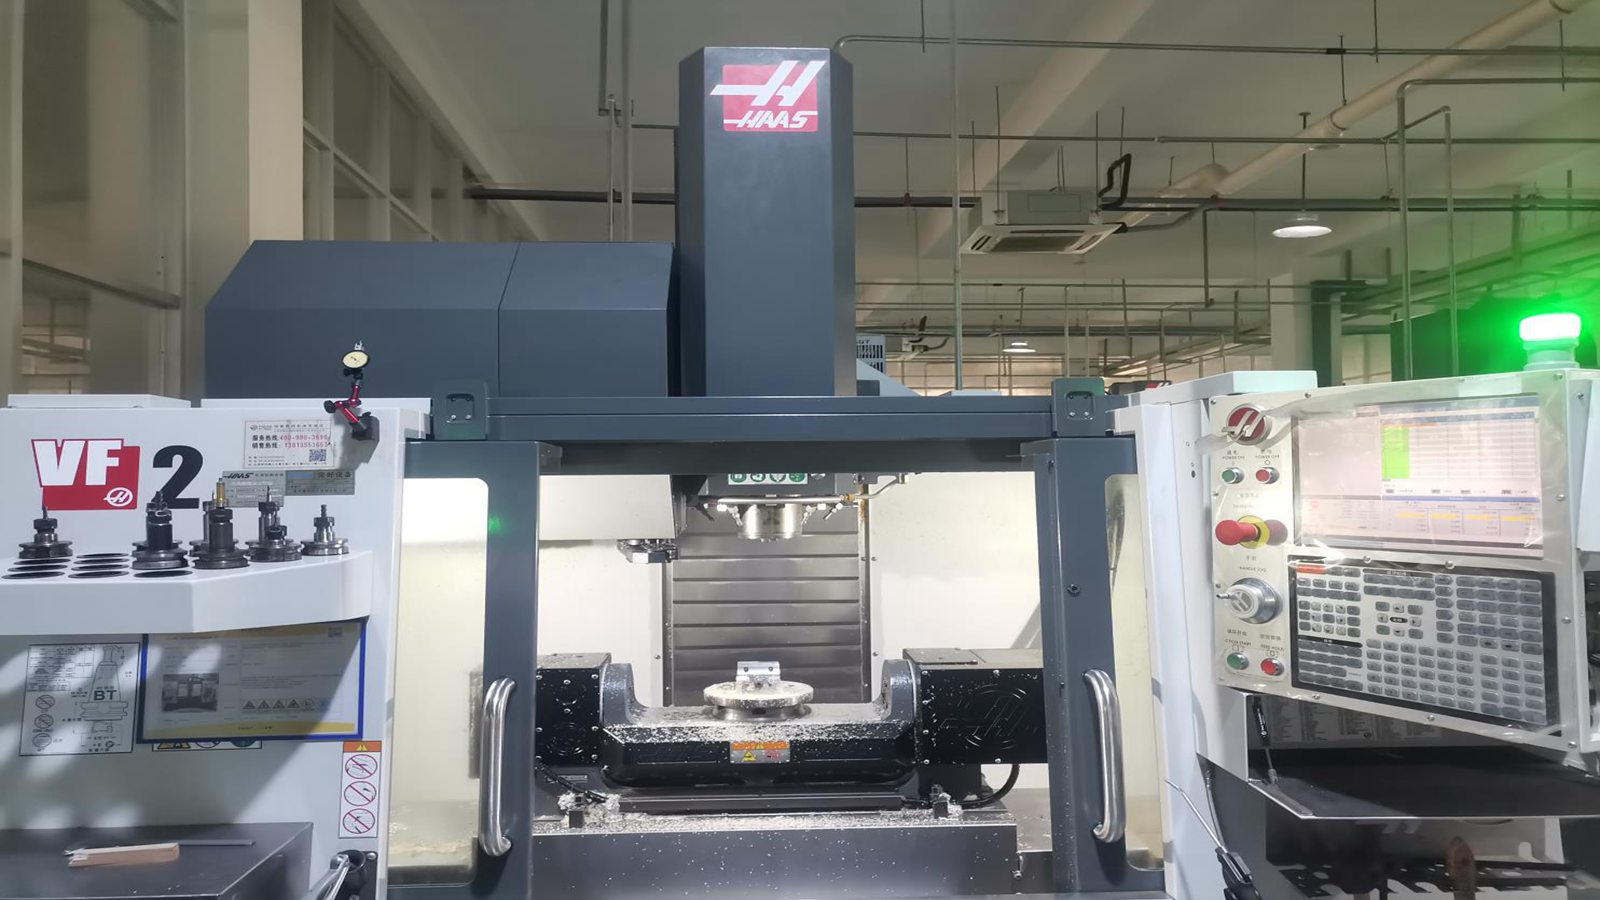
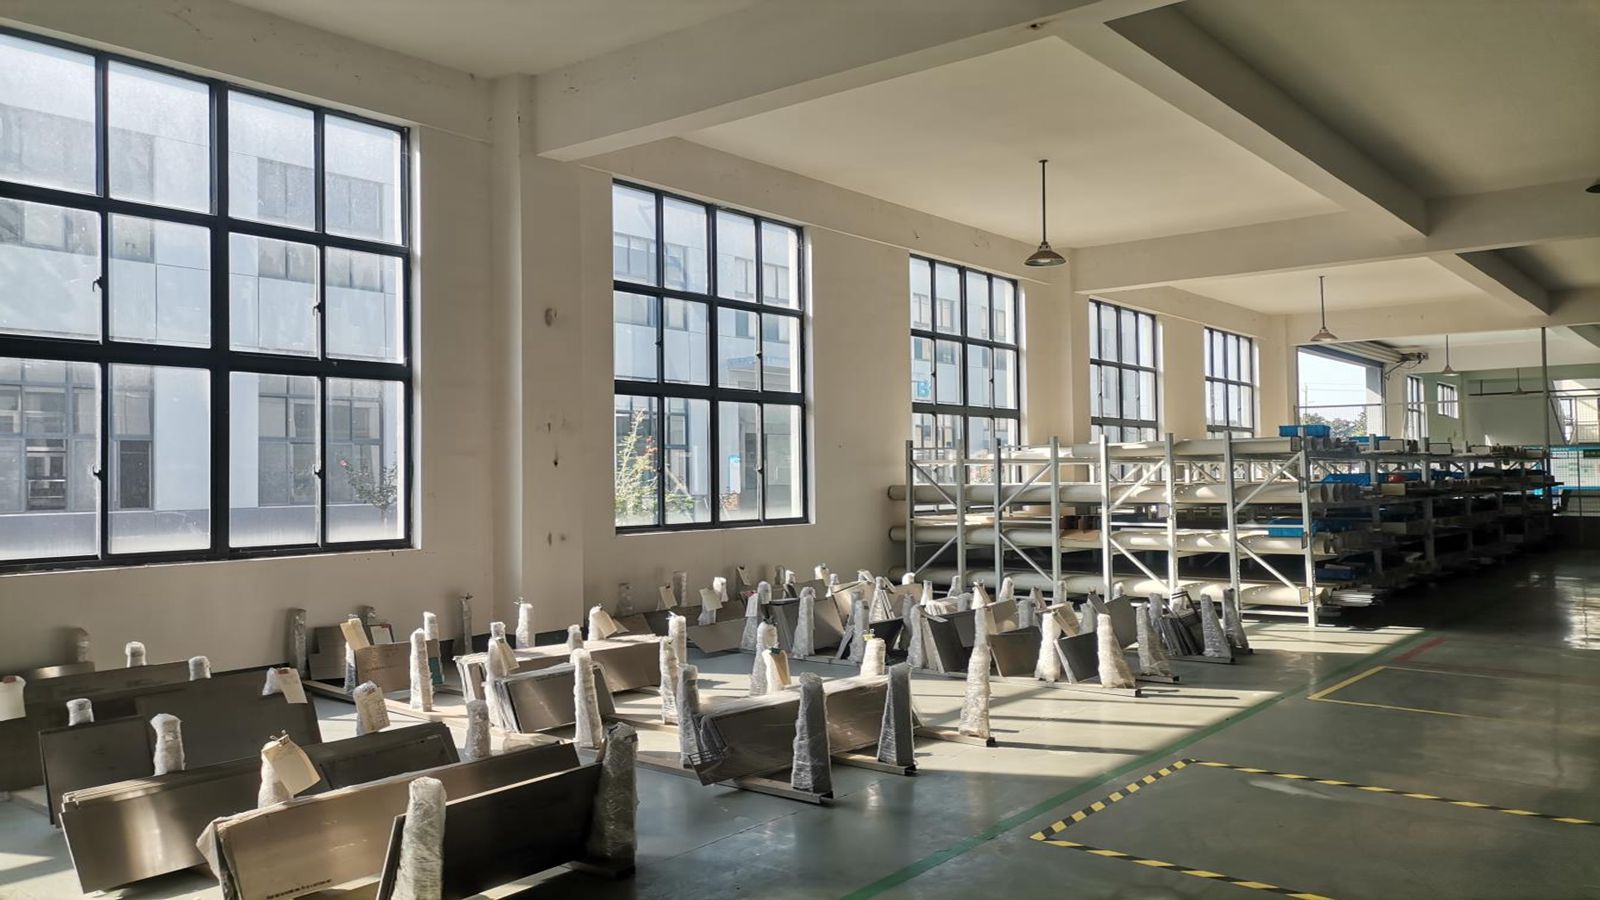
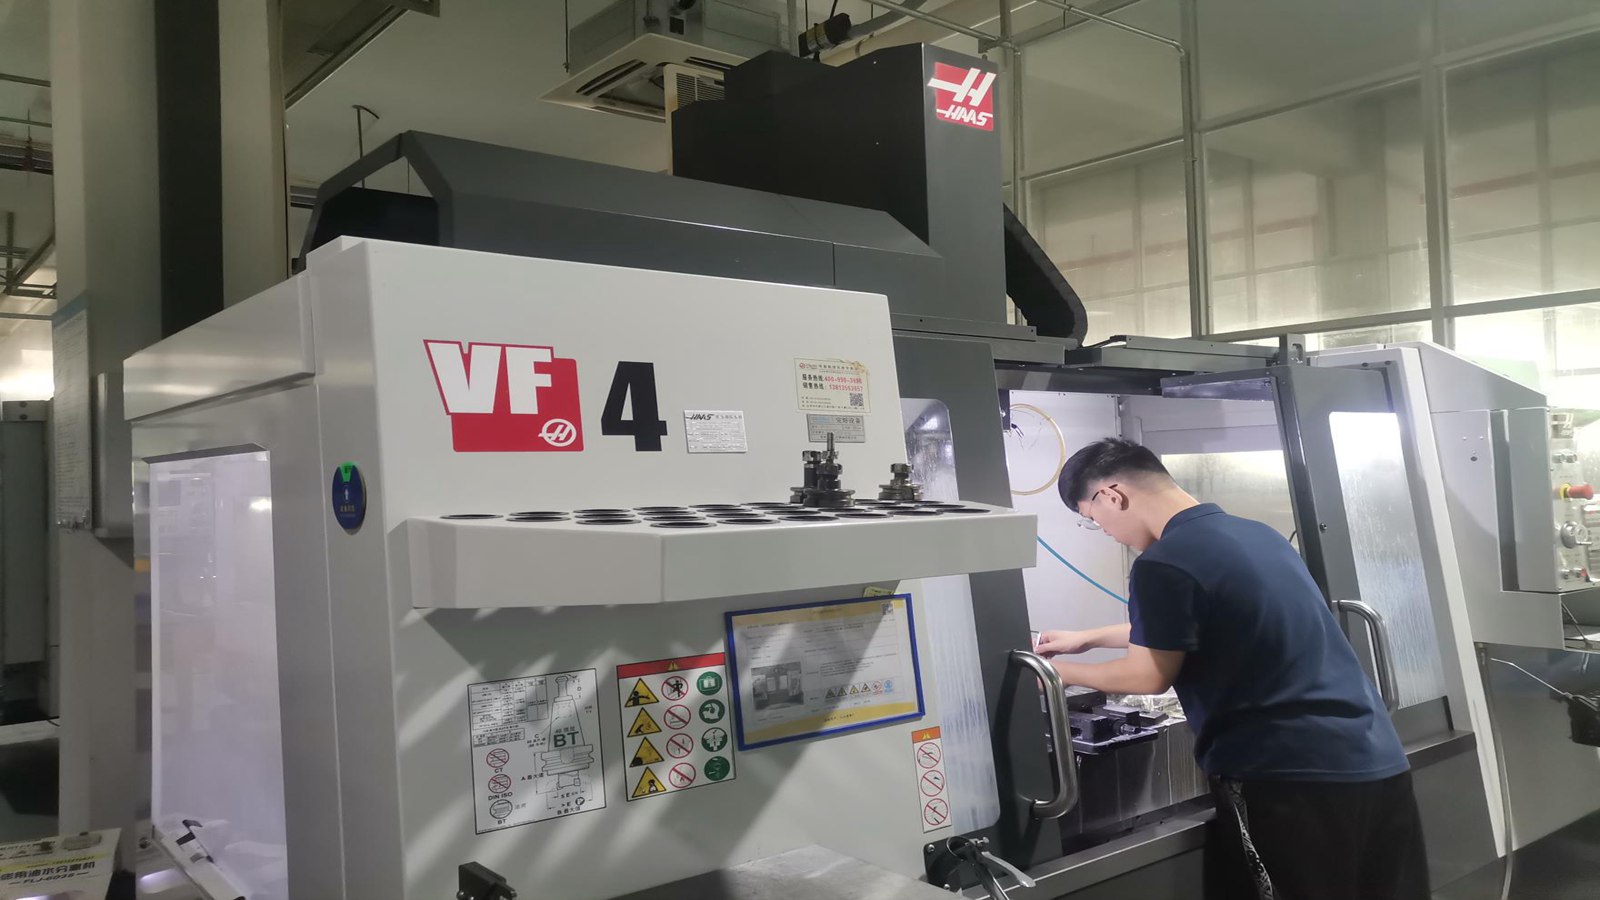
Operating out of a sprawling production facility exceeding 30,000 square meters, equipped with more than 350 advanced processing and testing machines, our industrial capacity is matched only by our dedication to precision. Our specialized orthopedic trolleys, surgical instrument sets, and modular implants are meticulously engineered to empower surgical teams, enhance workflow efficiency, and optimize patient outcomes in high-stakes operating room environments.
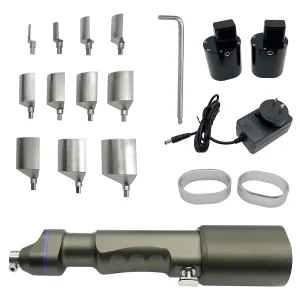
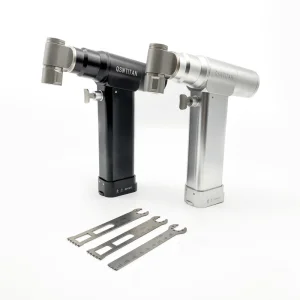
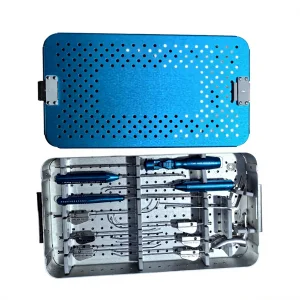
The global healthcare infrastructure is undergoing a massive transformation, driven by an aging demographic, rising incidence of musculoskeletal disorders, and an increased demand for minimally invasive orthopedic surgeries. Within this rapidly expanding market, specialized medical furniture—specifically orthopedic trolleys and instrument transit carts—plays a mission-critical role. Hospitals and ambulatory surgical centers worldwide require robust, corrosion-resistant, and ergonomically optimized trolleys capable of safely transporting heavy surgical sets, power tools, and high-precision implants directly into the sterile core.
China has emerged as the global epicenter for medical equipment manufacturing, propelled by state-of-the-art industrial clusters, streamlined supply chain logistics, and rigorous adherence to international regulatory standards such as ISO 13485, MDSAP, and CE MDR compliance. As a leading supplier, HBM leverages this geographic and technological advantage to deliver premium-grade orthopedic trolleys and surgical kits that rival legacy Western brands in durability while offering unmatched cost-efficiency for international distributors, group purchasing organizations (GPOs), and hospital networks.
At HBM Medical, quality is not merely an inspection checkpoint; it is deeply embedded across every phase of design, prototyping, CNC machining, surface treatment, and final sterilization packaging. Backed by 36 dedicated QA/QC inspectors and 12 fully optimized production lines featuring 120 precision machines, we ensure complete traceability of raw materials from certified metallurgy suppliers.
Our engineering division, comprised of 31 elite R&D professionals—including postgraduates, master graduates, and doctoral specialists—continuously introduces innovative product lines (25 new innovations launched last year alone). Whether fulfilling OEM/ODM customization requests, graphic processing, or tailor-made instrument sets, HBM maintains absolute compliance with global benchmarks, securing ISO 13485, MDSAP, and Class III CE certifications.
Our products and manufacturing facilities are fully certified by leading global bodies, holding ISO 13485 quality management certification, MDSAP, and Class III CE MDR certifications, guaranteeing compliance with stringent European and global medical regulations.
Yes. With robust R&D capabilities comprising 31 engineers and advanced production machinery, we specialize in OEM/ODM customization, sample processing, graphic processing, and bespoke surgical tray configurations.
We maintain full raw material batch traceability. Every production line undergoes strict quality oversight conducted by our team of 36 dedicated QA/QC inspectors, utilizing comprehensive inspection and testing protocols.
We collaborate with a diverse spectrum of global partners including medical device brand businesses, regional healthcare distributors, surgical engineers, hospital wholesalers, and medical equipment manufacturers.
 HBM Medical