
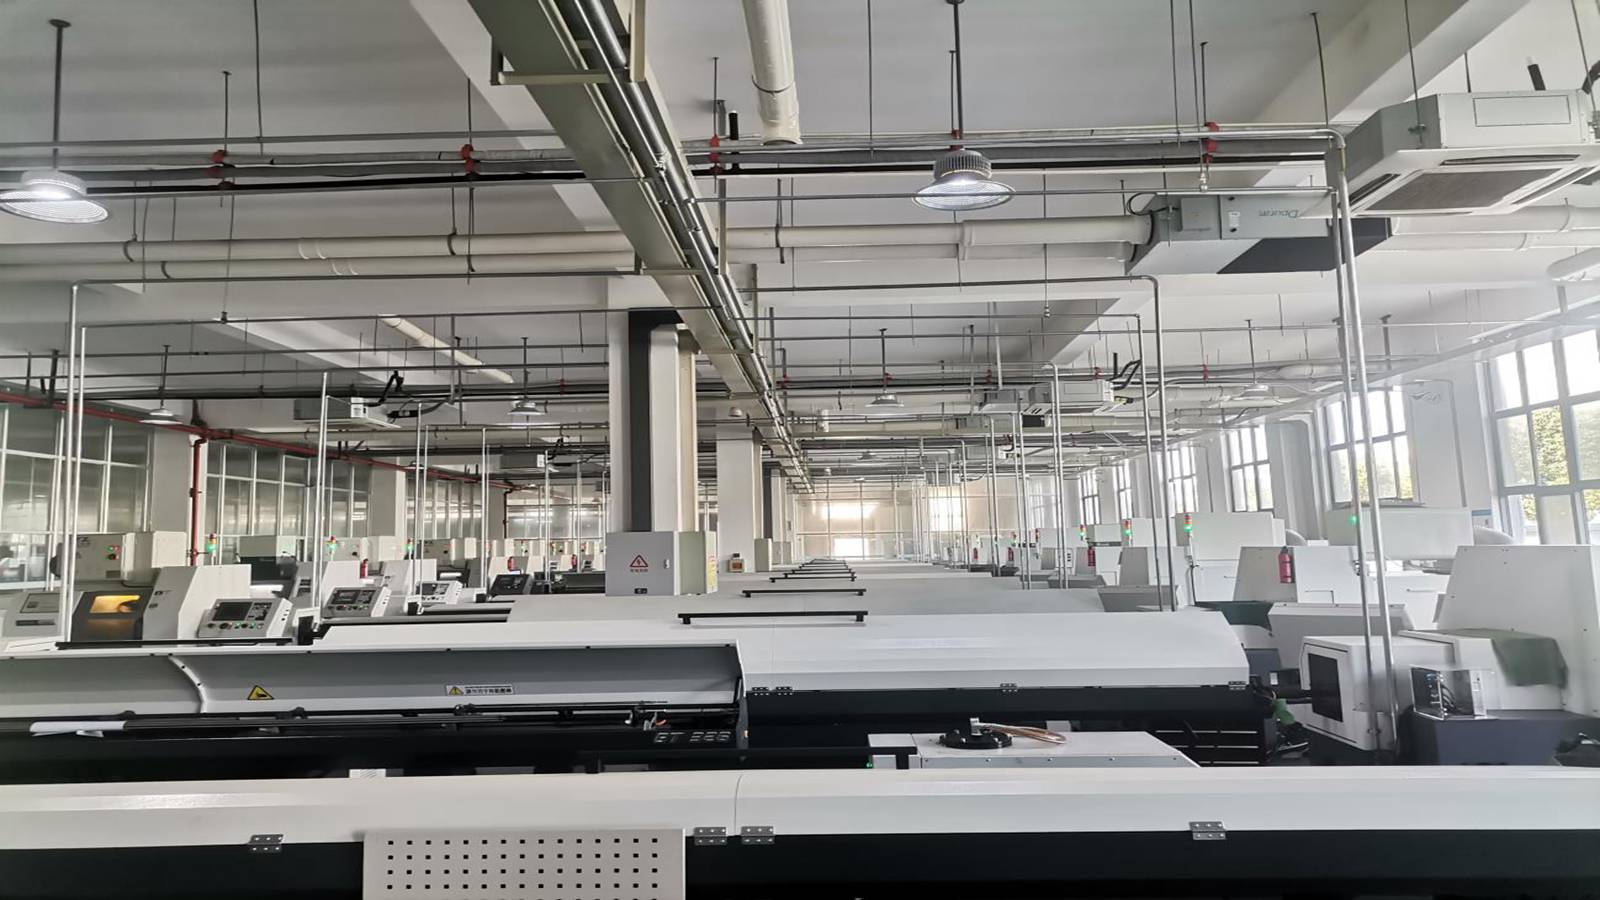
Advanced Manufacturing Facility
Precision Processing & Testing Machines
Years of Global Export Experience
Dedicated QA/QC Inspectors
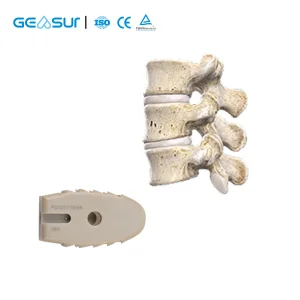
HBM Medical Apparatus And Instruments Co., Ltd. stands at the forefront of the global orthopedic medical equipment industry. Established with a vision to integrate medical mastery and achieve supreme patient health, HBM has emerged as a premier R&D, manufacturing, and operation enterprise based in China. Specializing in advanced spinal solutions, particularly PEEK and titanium orthopedic cages, our footprint spans domestic markets and extends to Eastern Europe, Southeast Asia, and beyond.
Orthopedic cages—vital interbody fusion devices used in spinal stabilization surgeries—have undergone profound technological shifts. Modern surgical procedures demand implants that not only restore disc height and neural foraminal volume but also promote biological osteointegration. By leveraging cutting-edge computer-aided design (CAD) and stringent quality frameworks conforming to ISO 13485, CE, MDSAP, and FDA standards, HBM ensures each cage delivers optimal biomechanical stability and long-term clinical success.
International healthcare providers and distributors increasingly seek ISO and CE-certified spinal implants from China to balance rigorous clinical efficacy with cost-efficiency. Our scalable production capacity ensures continuous supply chain resilience for global partners.
We provide comprehensive integrated solutions covering everything from raw material metallurgical traceability to sterile-packaged final implants, reducing time-to-market for OEM/ODM brand businesses and medical distributors.
Driven by 31 specialized R&D engineers—including doctoral and post-graduate experts—we launched 25 new products last year, focusing on minimally invasive spine (MIS) systems and patient-specific anatomical matching.
Adhering to Google’s stringent E-E-A-T (Experience, Expertise, Authoritativeness, Trustworthiness) criteria, HBM Medical combines academic excellence with industrial manufacturing might. Our production site houses over 120 precision machines across 12 dedicated production lines. Every single batch undergoes rigorous 100% full inspection or stringent AQL random sampling conducted by our 36 certified QA/QC specialists.
We offer customized manufacturing solutions, supporting graphic processing, sample processing, and tailor-made dimensional requirements to suit diverse ethnic anatomical variations across global markets. Our compliance portfolio—featuring CE MDR certifications and strict raw material traceability—guarantees absolute regulatory security for hospital procurement committees and surgical teams worldwide.
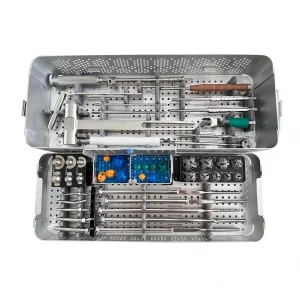
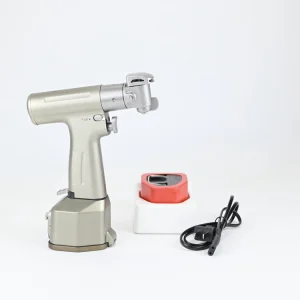
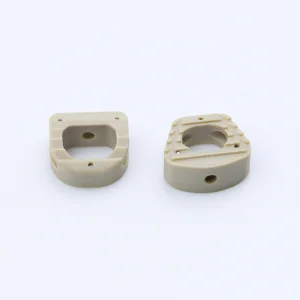
Our expansive 30,343-square-meter facility houses state-of-the-art CNC machining centers, cleanroom packaging zones, and advanced metrology laboratories designed to maintain uncompromising quality standards across all production lines.
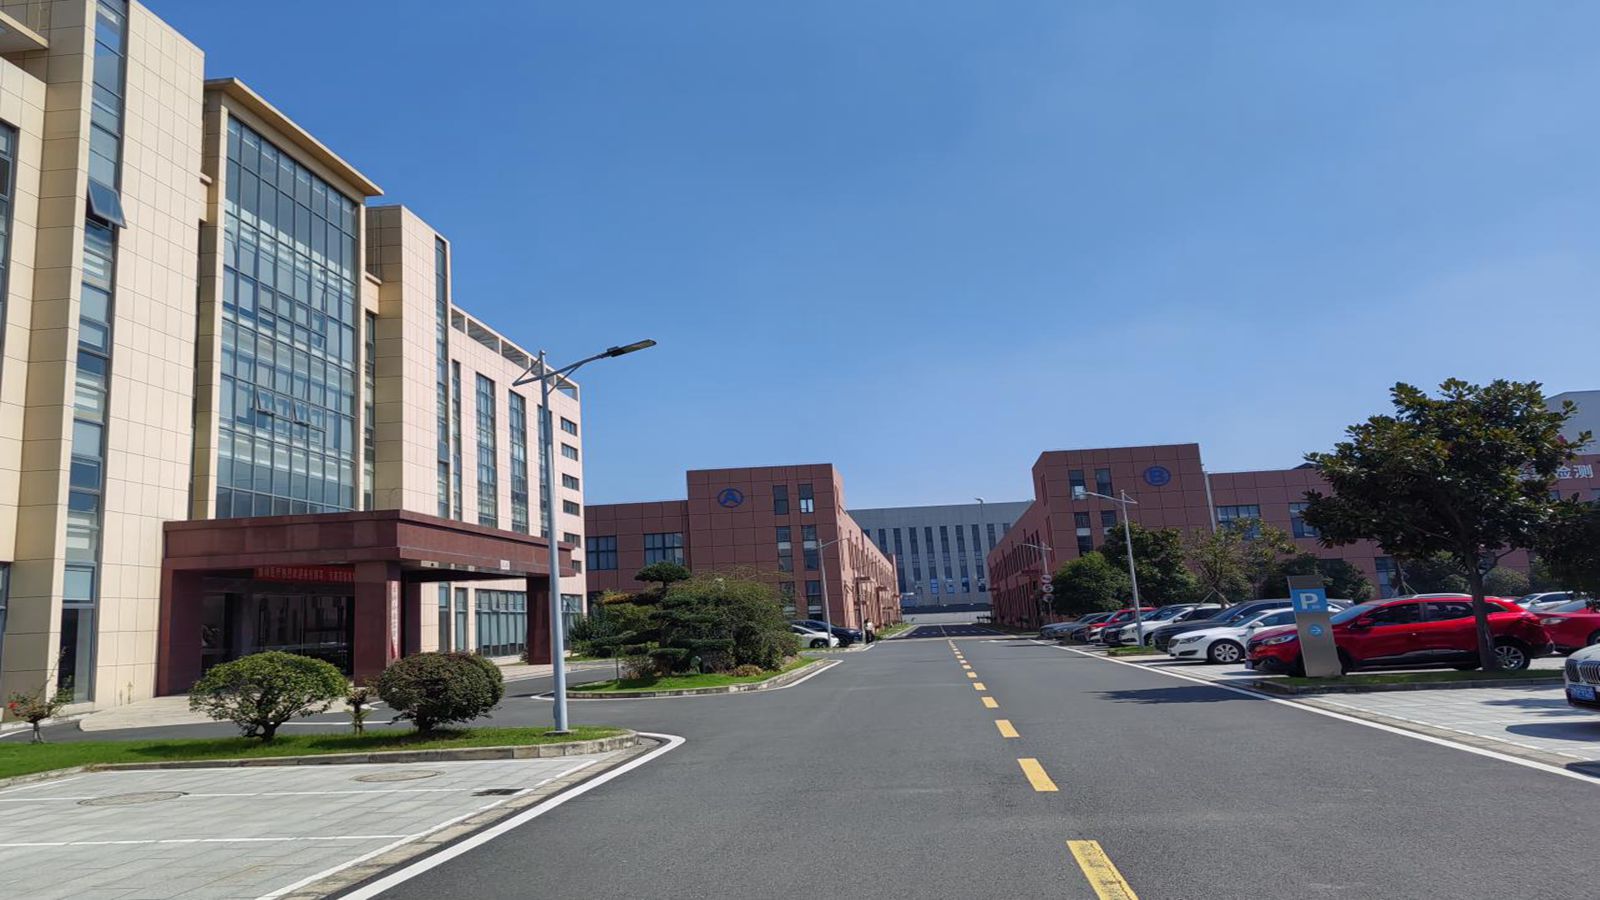
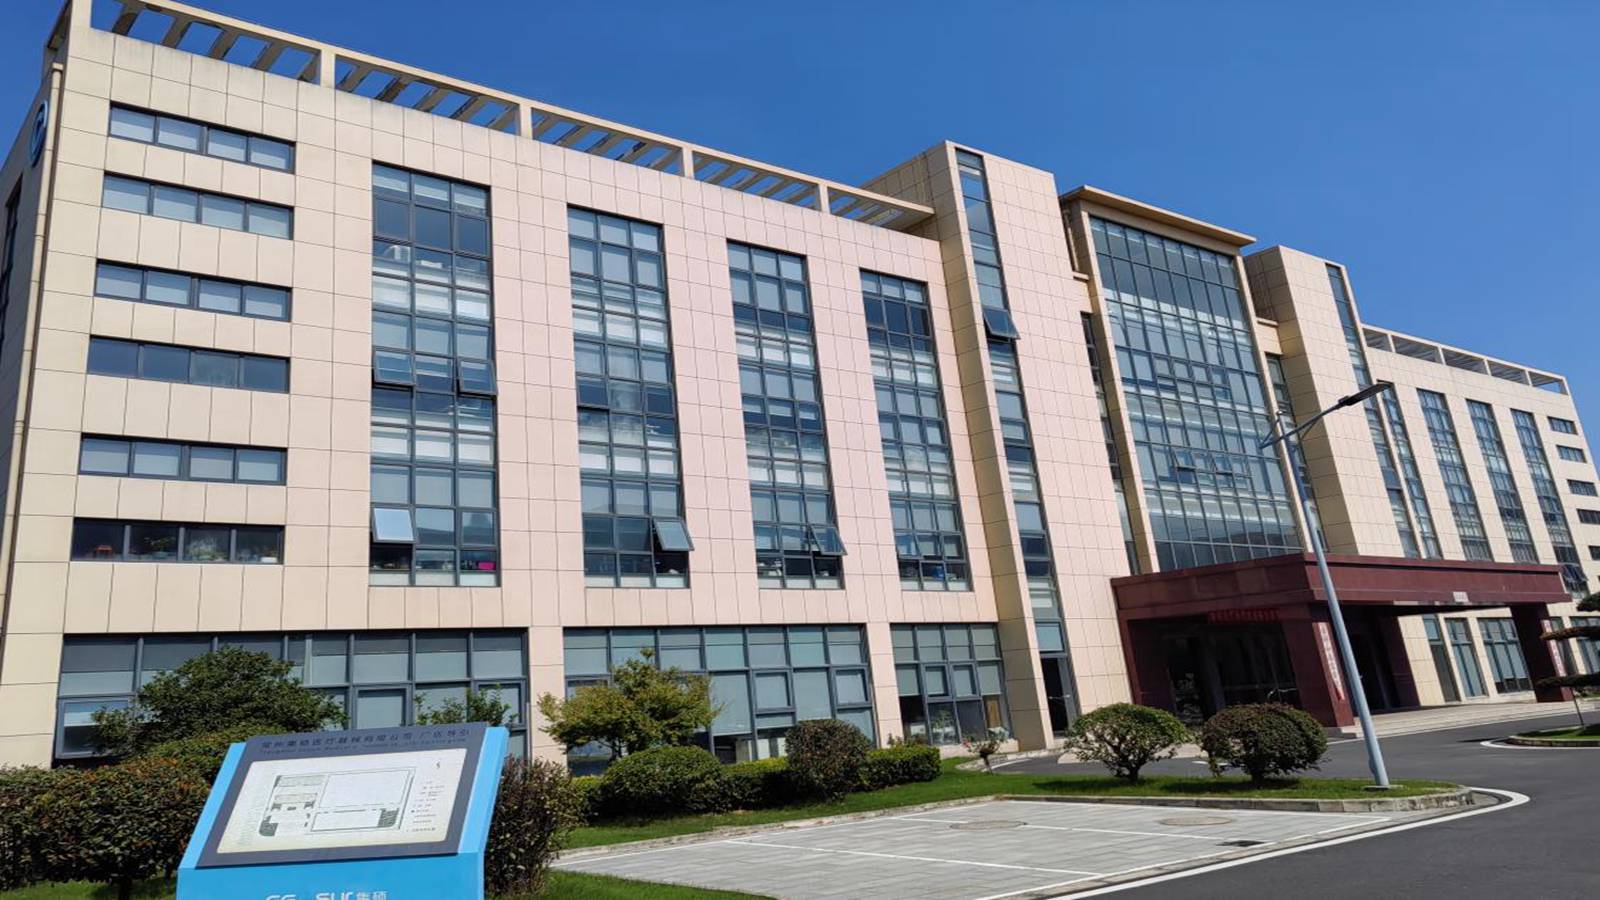
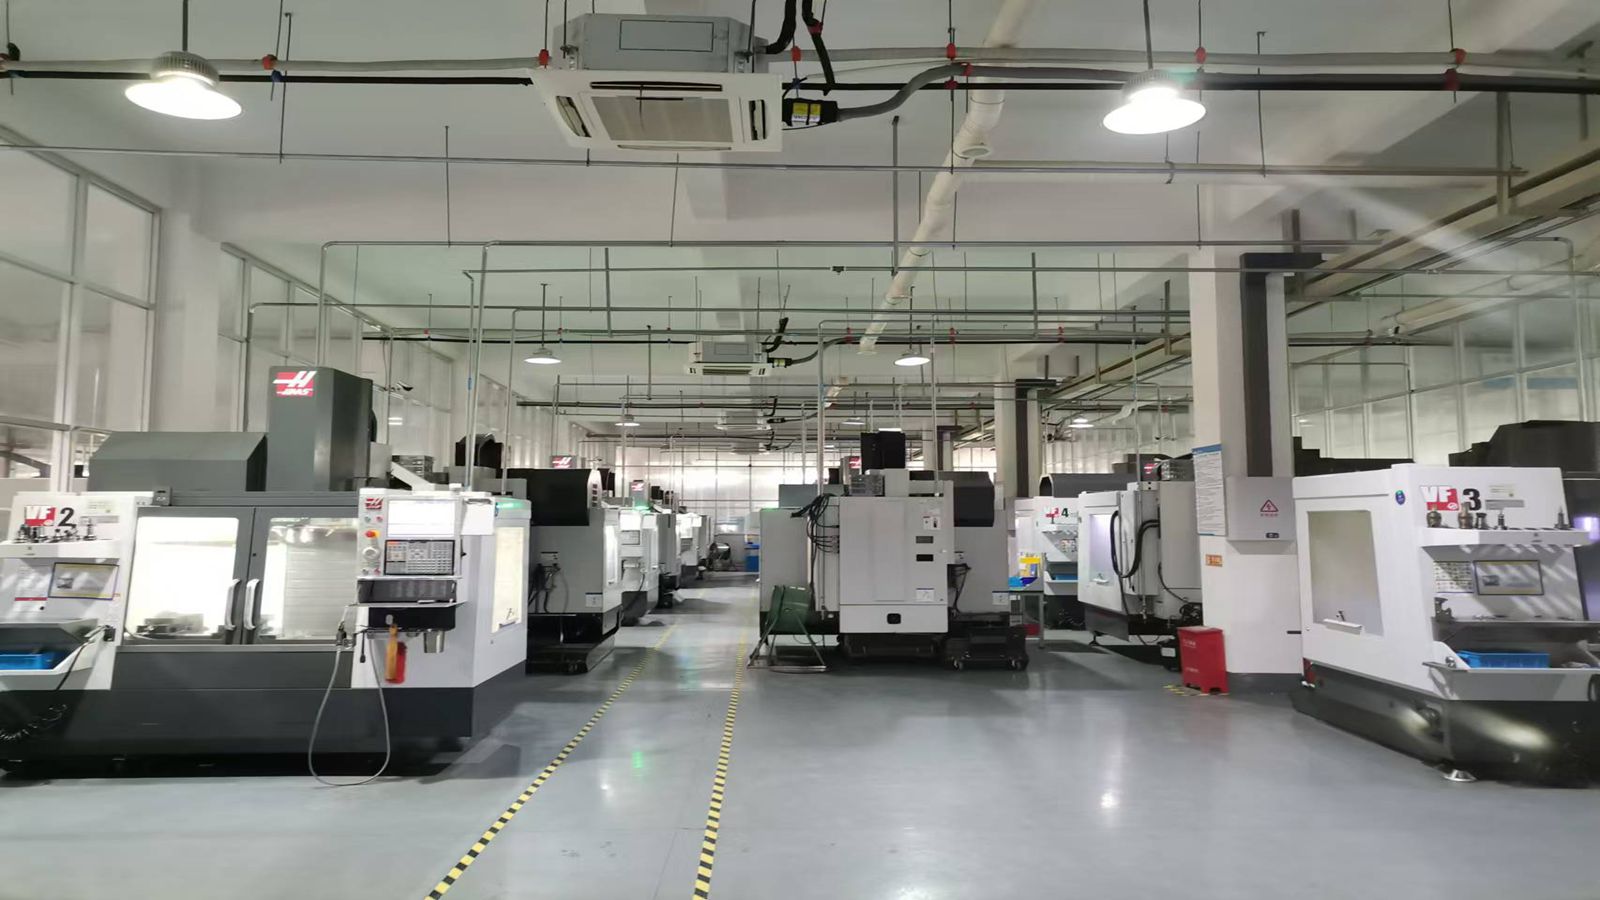
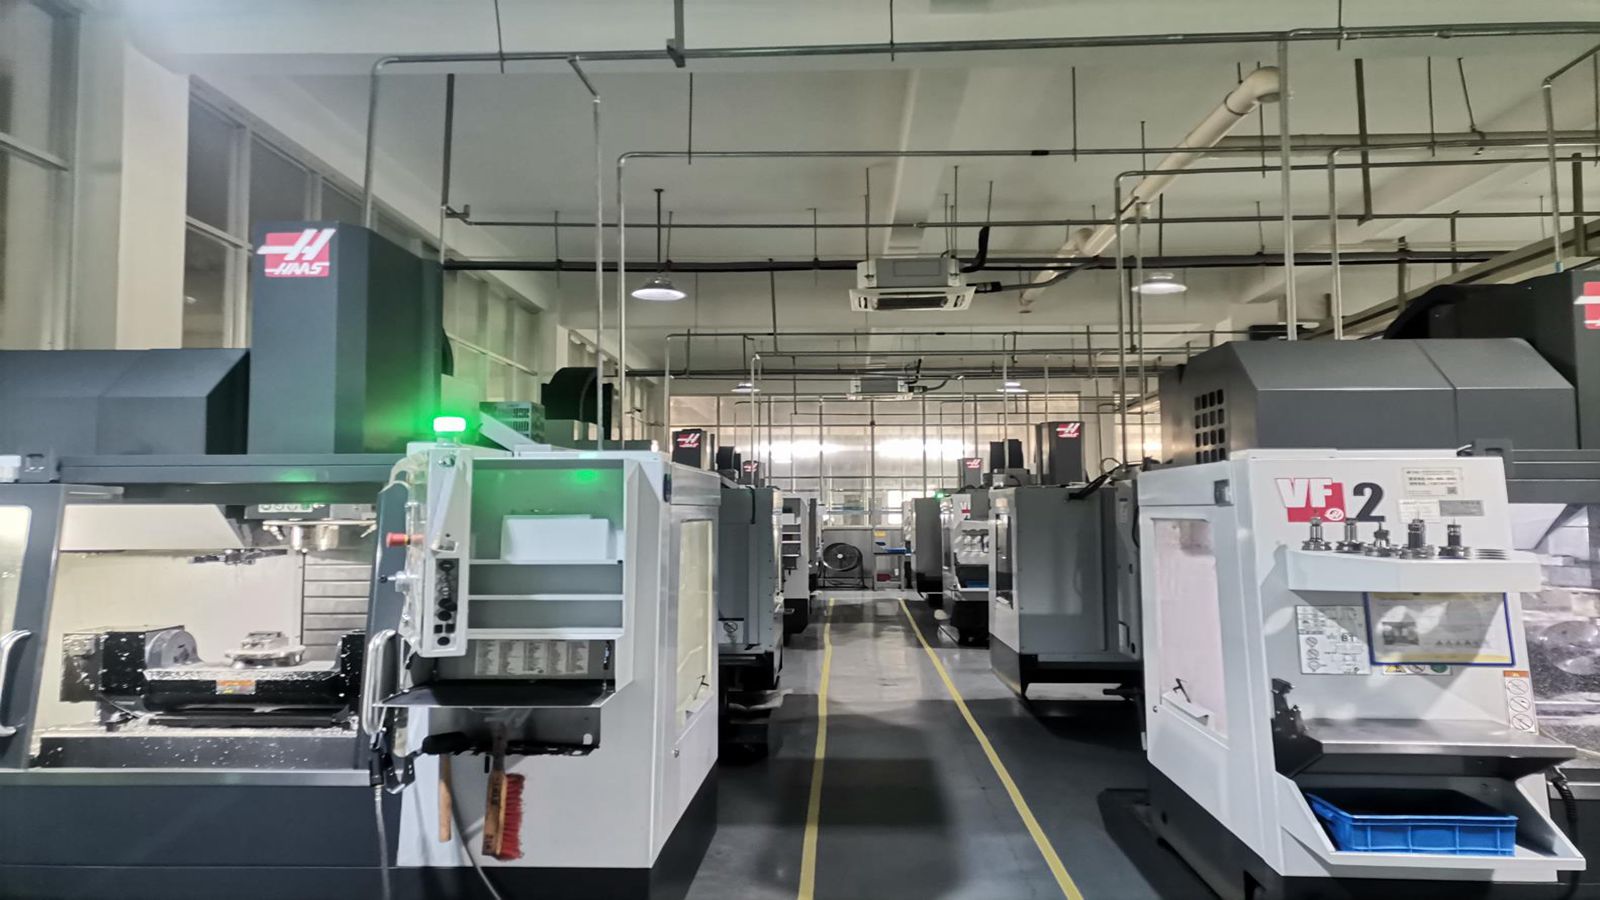
Our orthopedic implants and cages are manufactured under strict ISO 13485 quality management systems and hold major international credentials including CE MDR certifications, MDSAP, and full compliance with FDA benchmarks.
Yes. With 31 experienced R&D engineers holding advanced degrees (including post-graduates and doctorates), we specialize in OEM/ODM partnerships, graphic processing, sample processing, and custom-dimension implant manufacturing tailored to specific clinical requirements.
We primarily utilize medical-grade PEEK (Polyetheretherketone) known for its modulus elasticity close to human bone and radiolucency, as well as high-grade titanium alloys for enhanced structural stability and osteointegration.
We maintain 100% full raw material traceability. Our production floor features 120 advanced machines and is monitored by 36 dedicated QA/QC inspectors conducting rigorous product inspections across all 12 production lines.
 HBM Medical