Providing Grenville healthcare systems, surgical distributors, and trauma centers with high-precision titanium implants, PEEK cages, and custom-engineered spinal instrument sets.
Engineered to titanium Grade 5 ELI standards with micron-level tolerances for minimal invasive and open surgical procedures.
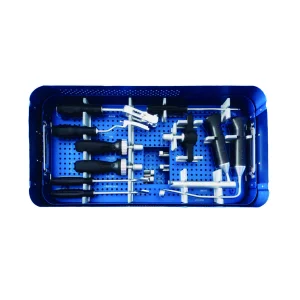
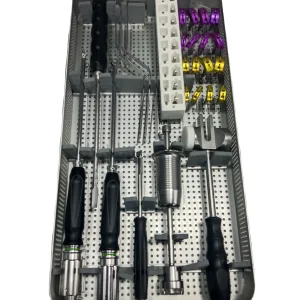
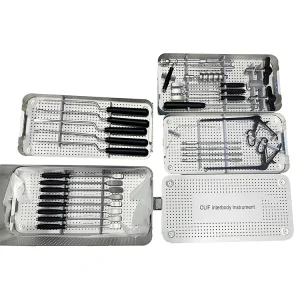
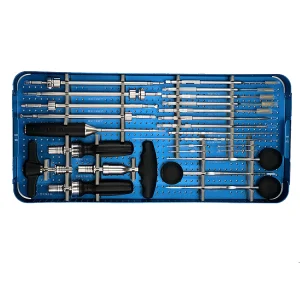
The global demand for high-precision orthopedic trauma hardware and spinal reconstruction systems has experienced an unprecedented shift toward centralized quality assurance and specialized manufacturing hubs. For regional medical networks, specialized surgical centers, and healthcare equipment distributors servicing the Grenville area, maintaining an unbroken supply chain of Class I and Class II medical devices is vital to meeting clinical demands.
In regions such as Grenville, healthcare providers are seeing an accelerated volume of degenerative disc disease treatments, complex thoracolumbar trauma interventions, and outpatient Minimally Invasive Surgery (MIS) procedures. Modern hospitals require instrument kits that deliver flawless mechanical feedback, corrosion resistance across thousands of autoclave cycles, and total dimensional uniformity.
Standard off-the-shelf catalog offerings frequently fail to address the specific ergonomic preferences of orthopedic surgeons or the exact sterilization tray configurations required by Grenville central sterile processing departments (SPD). Thus, direct factory collaboration with high-tier manufacturers capable of quick-turn custom CNC machining, laser marking, and customized tray layout becomes a strategic necessity.
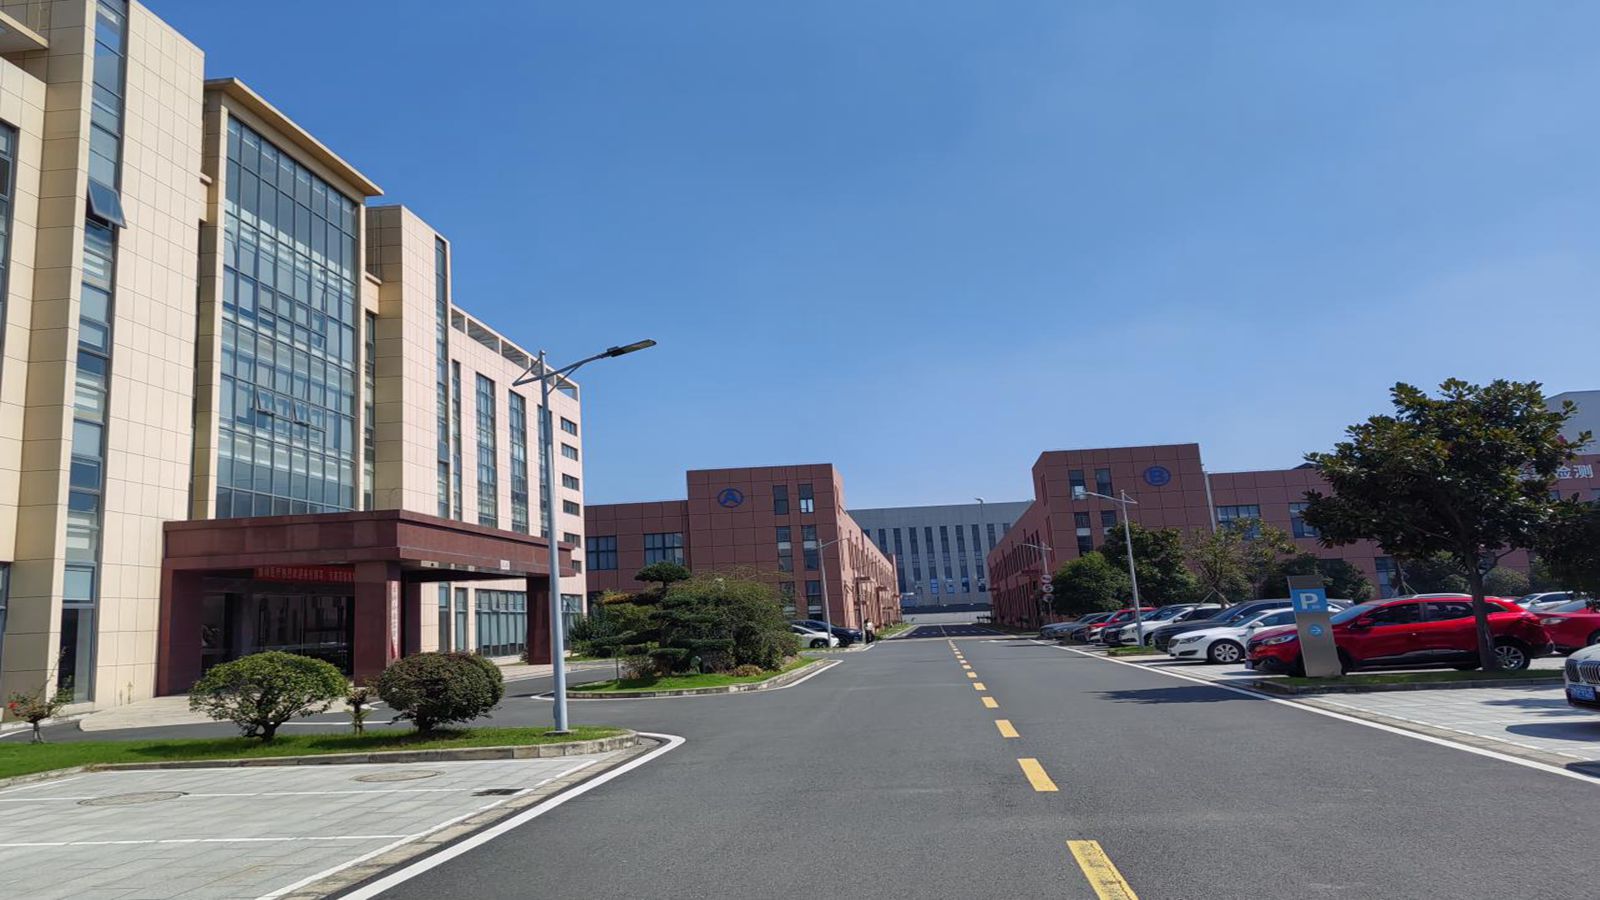
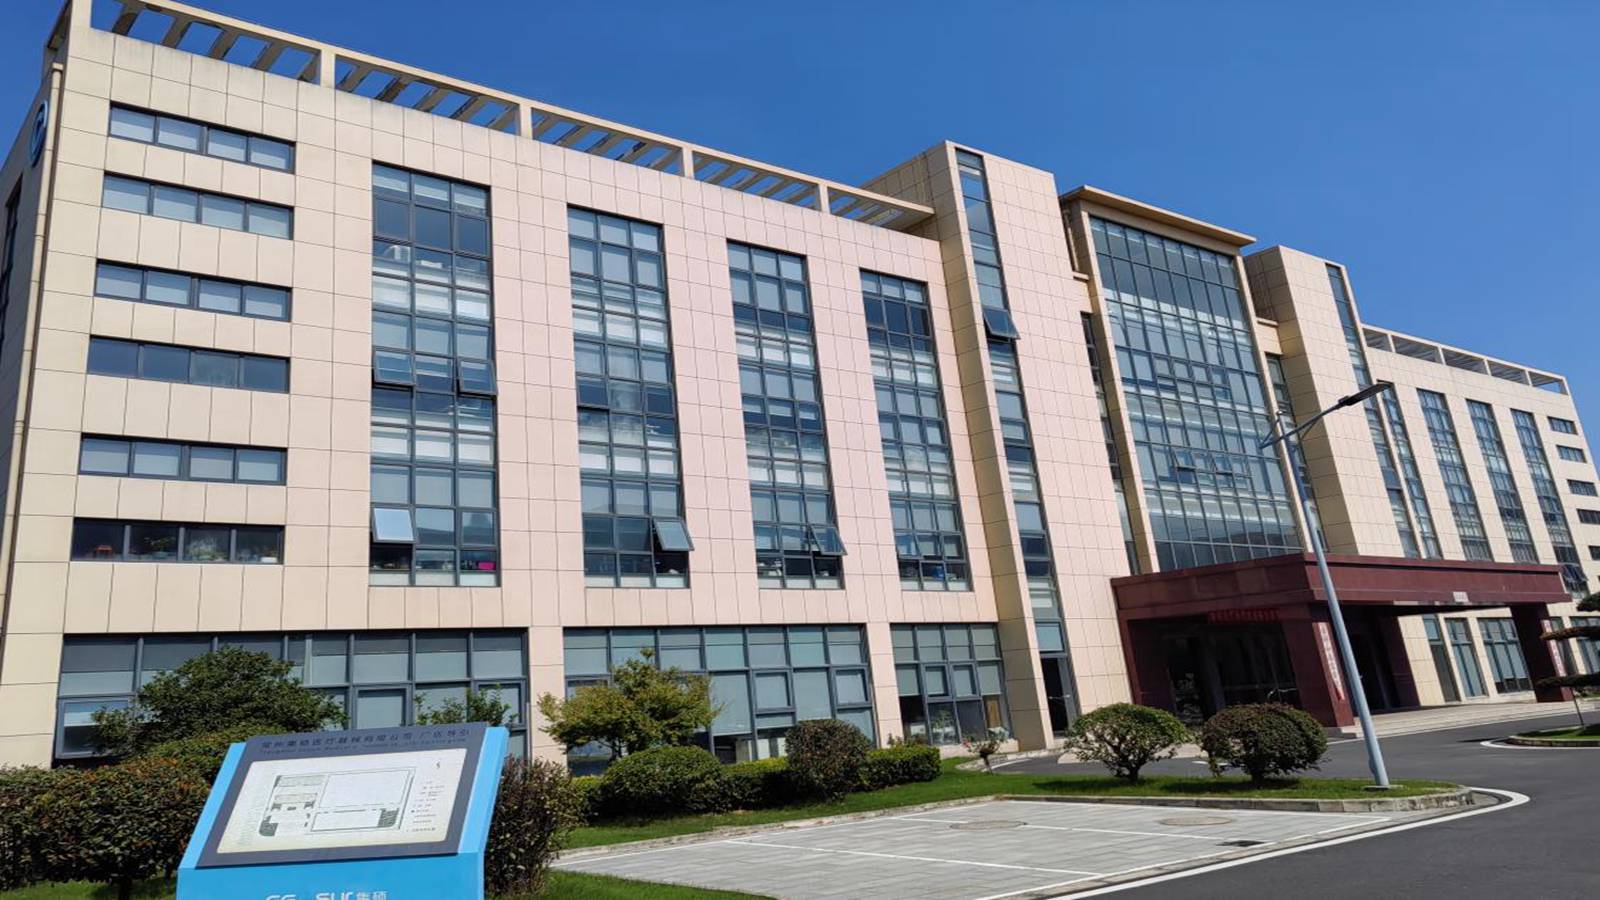
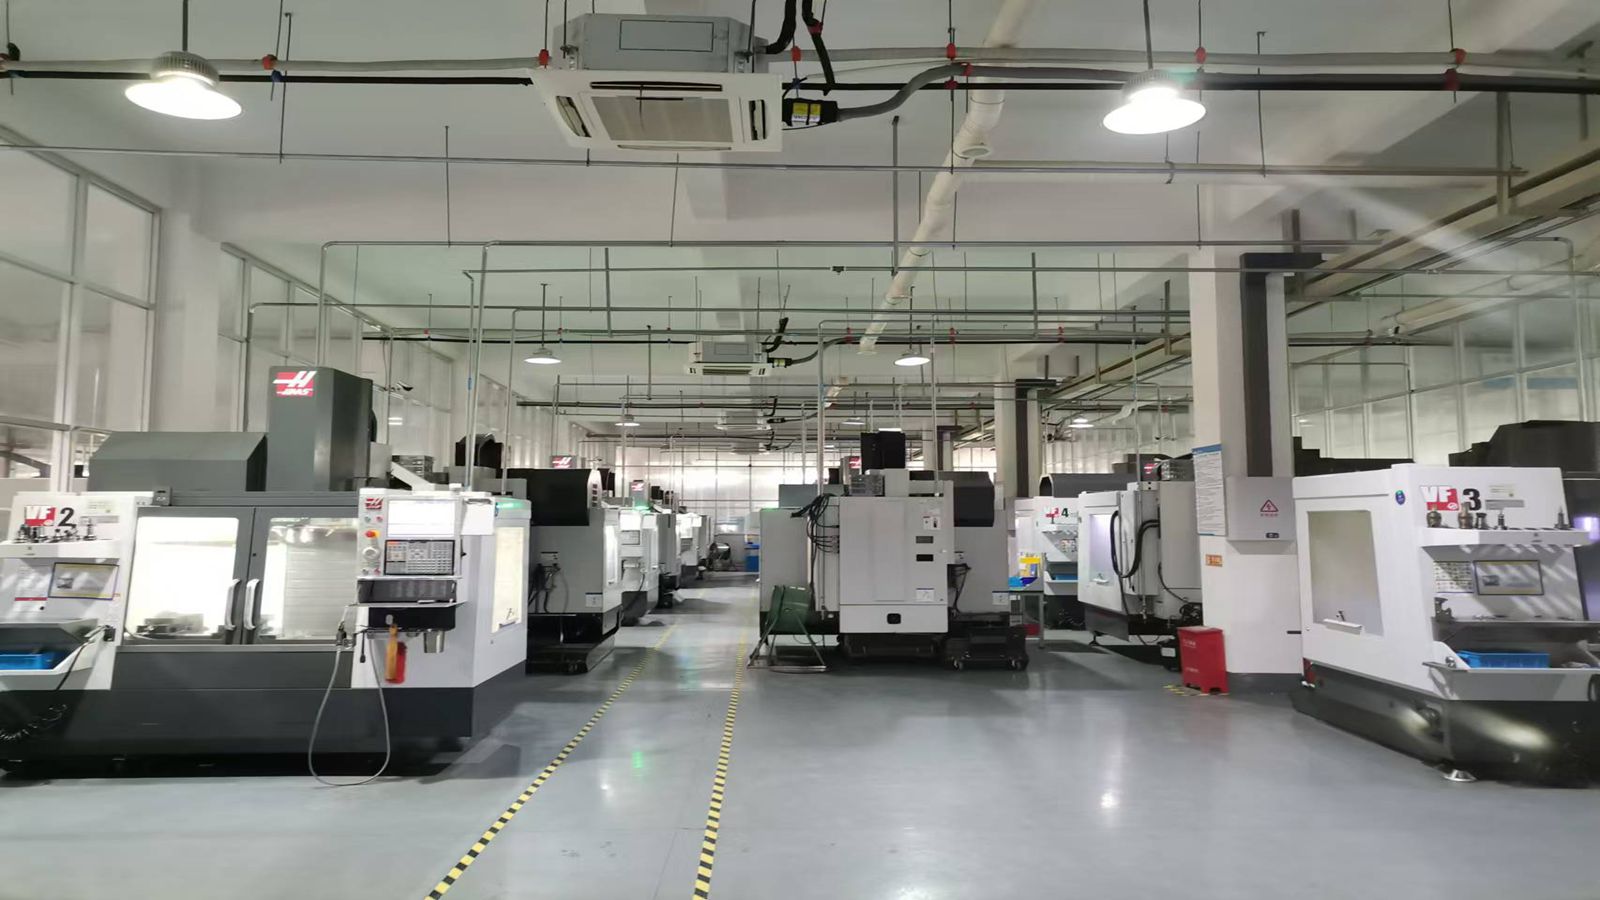
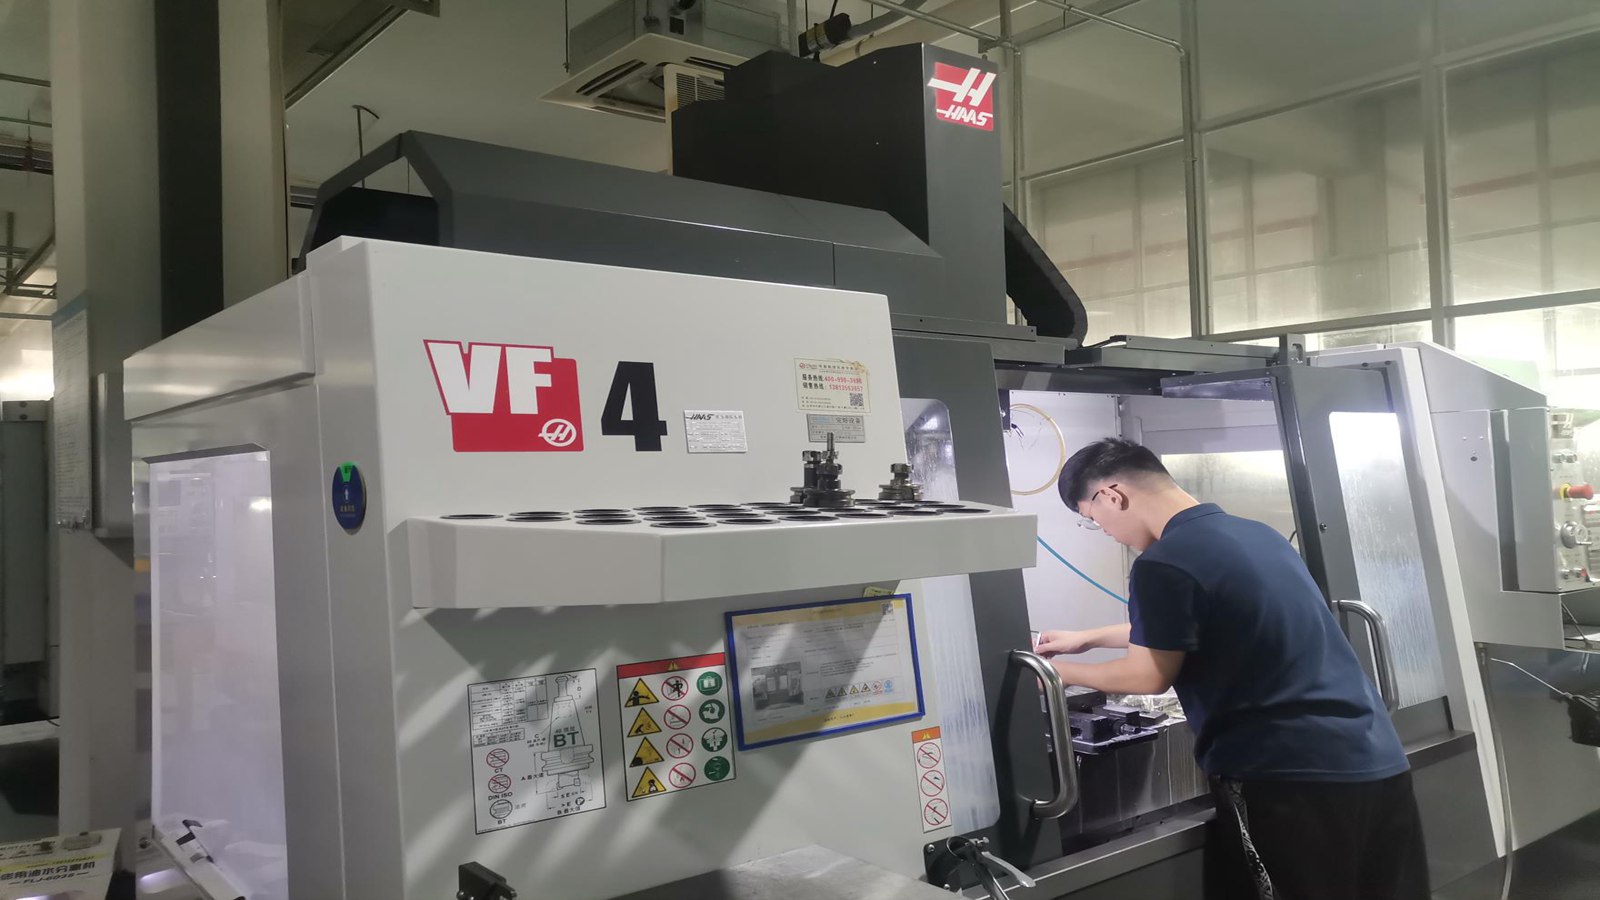
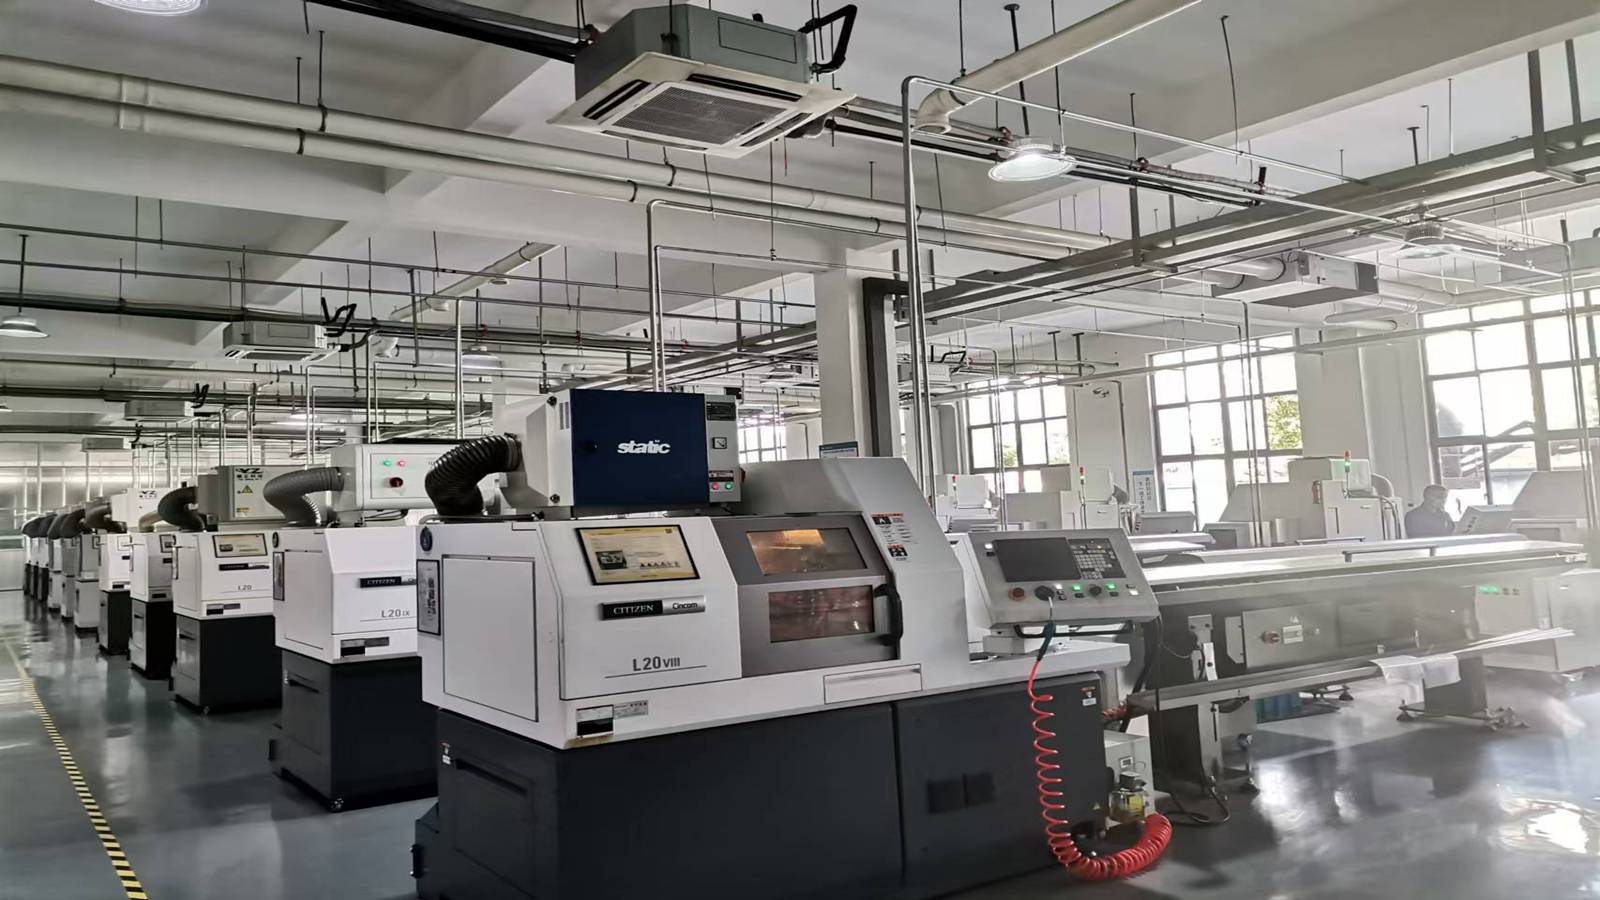
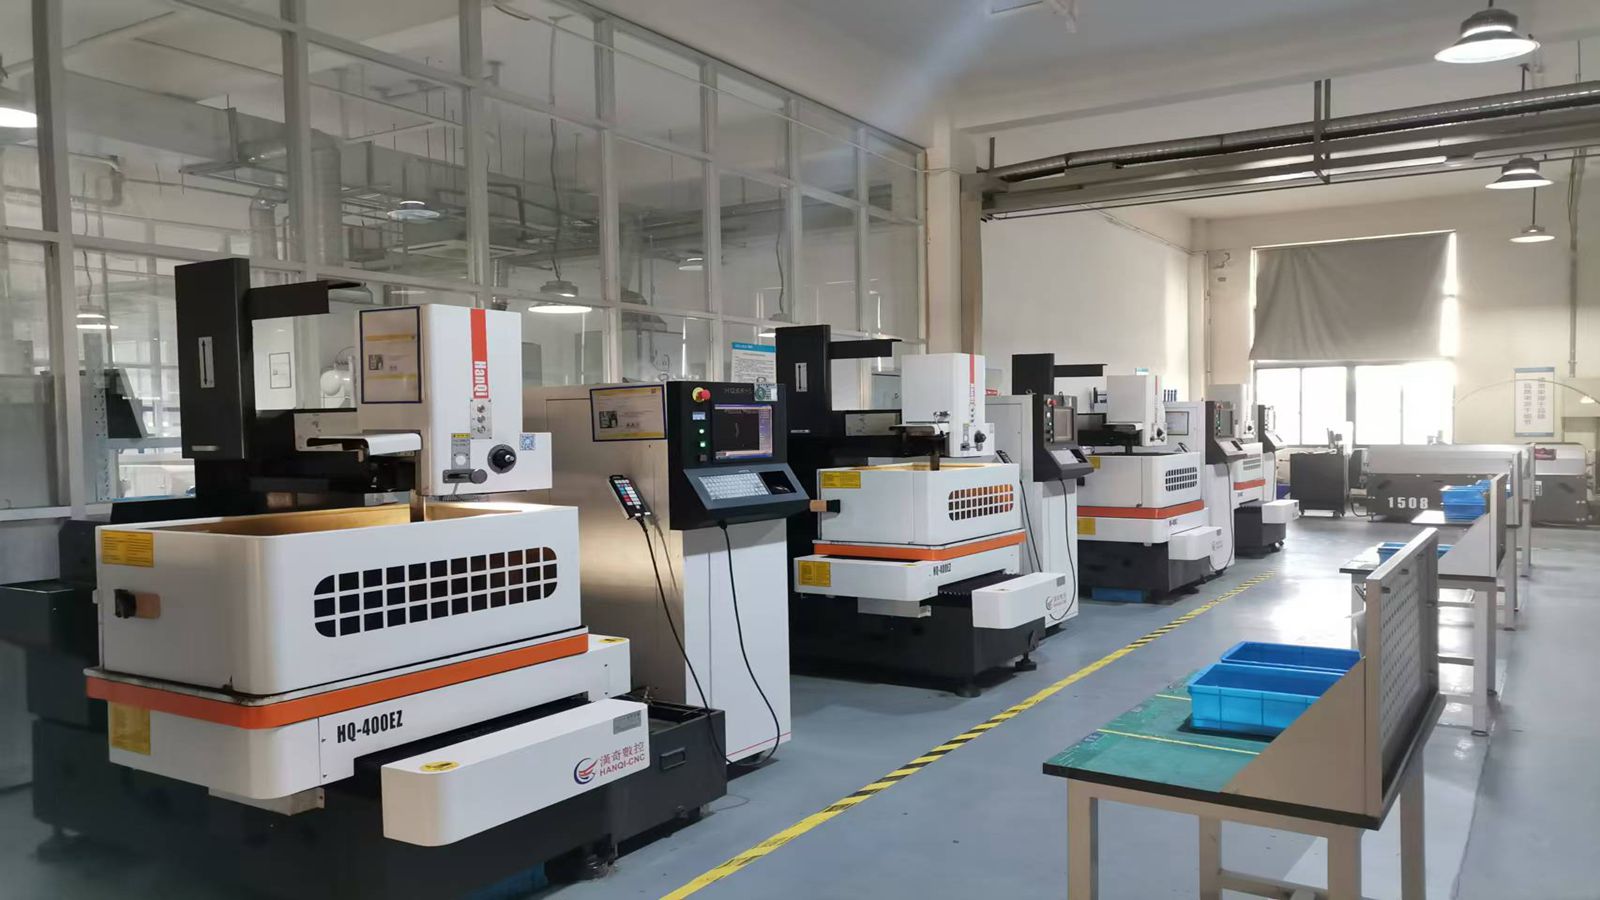
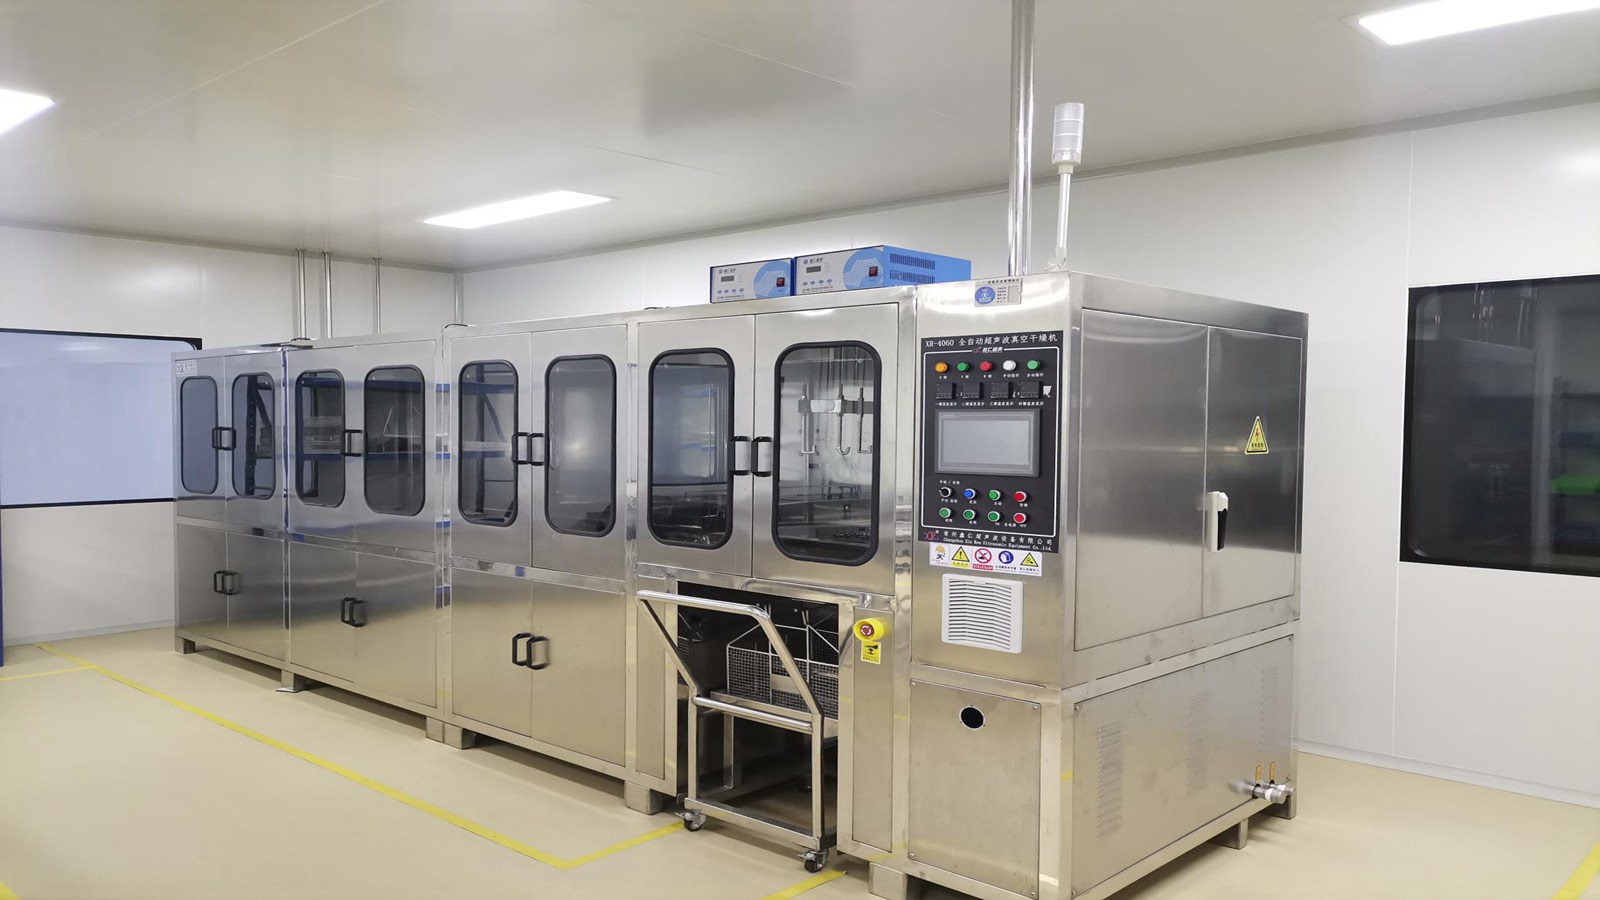
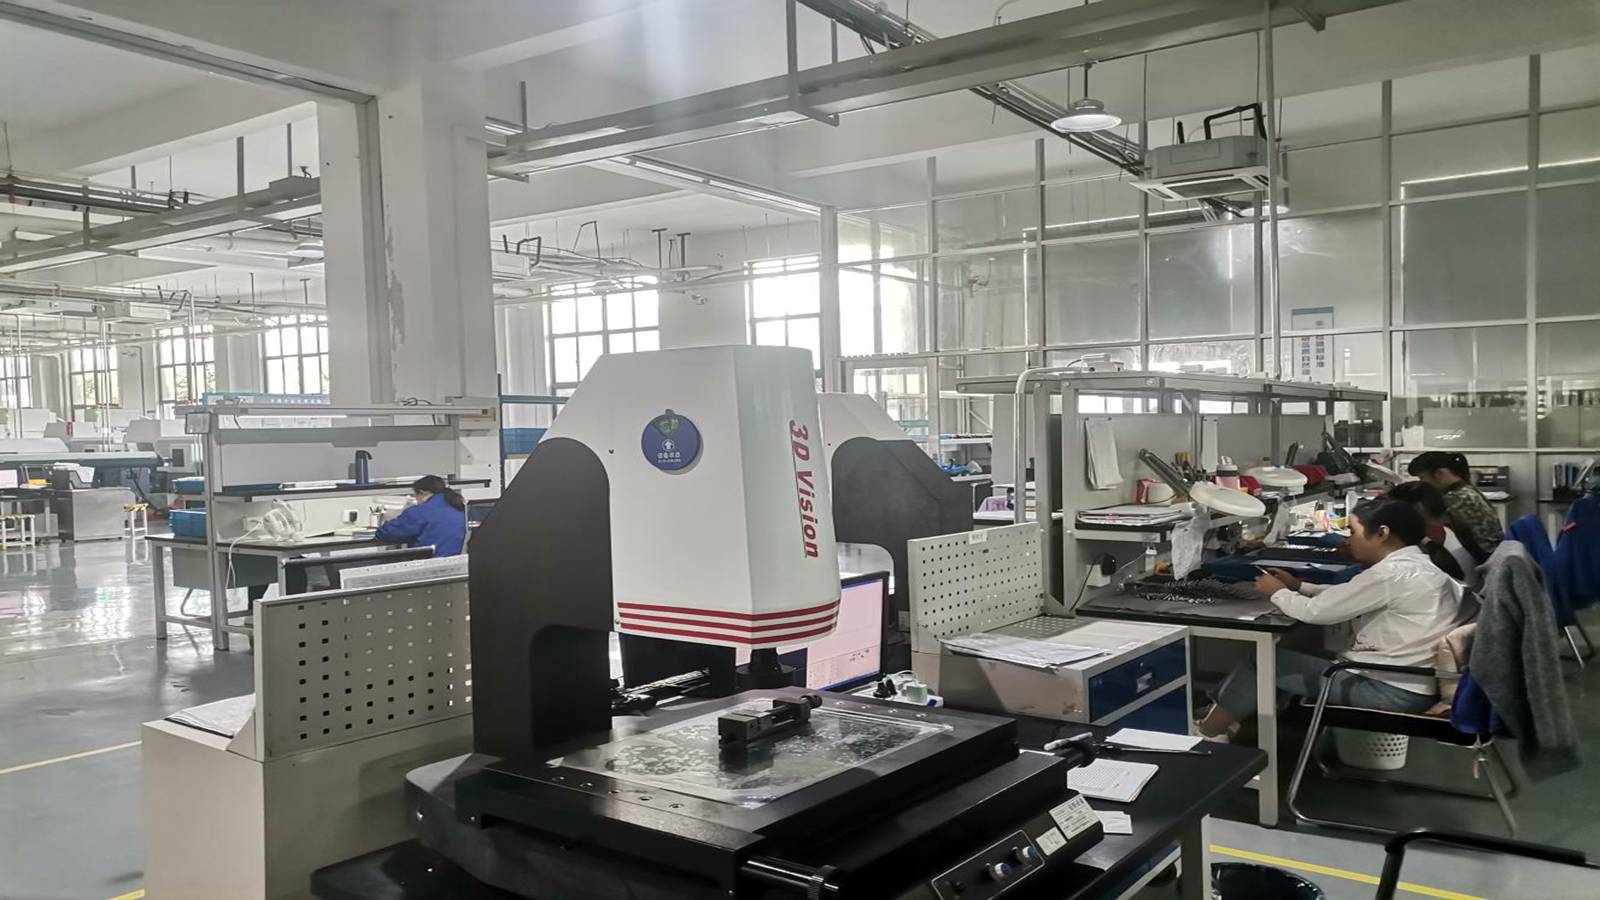
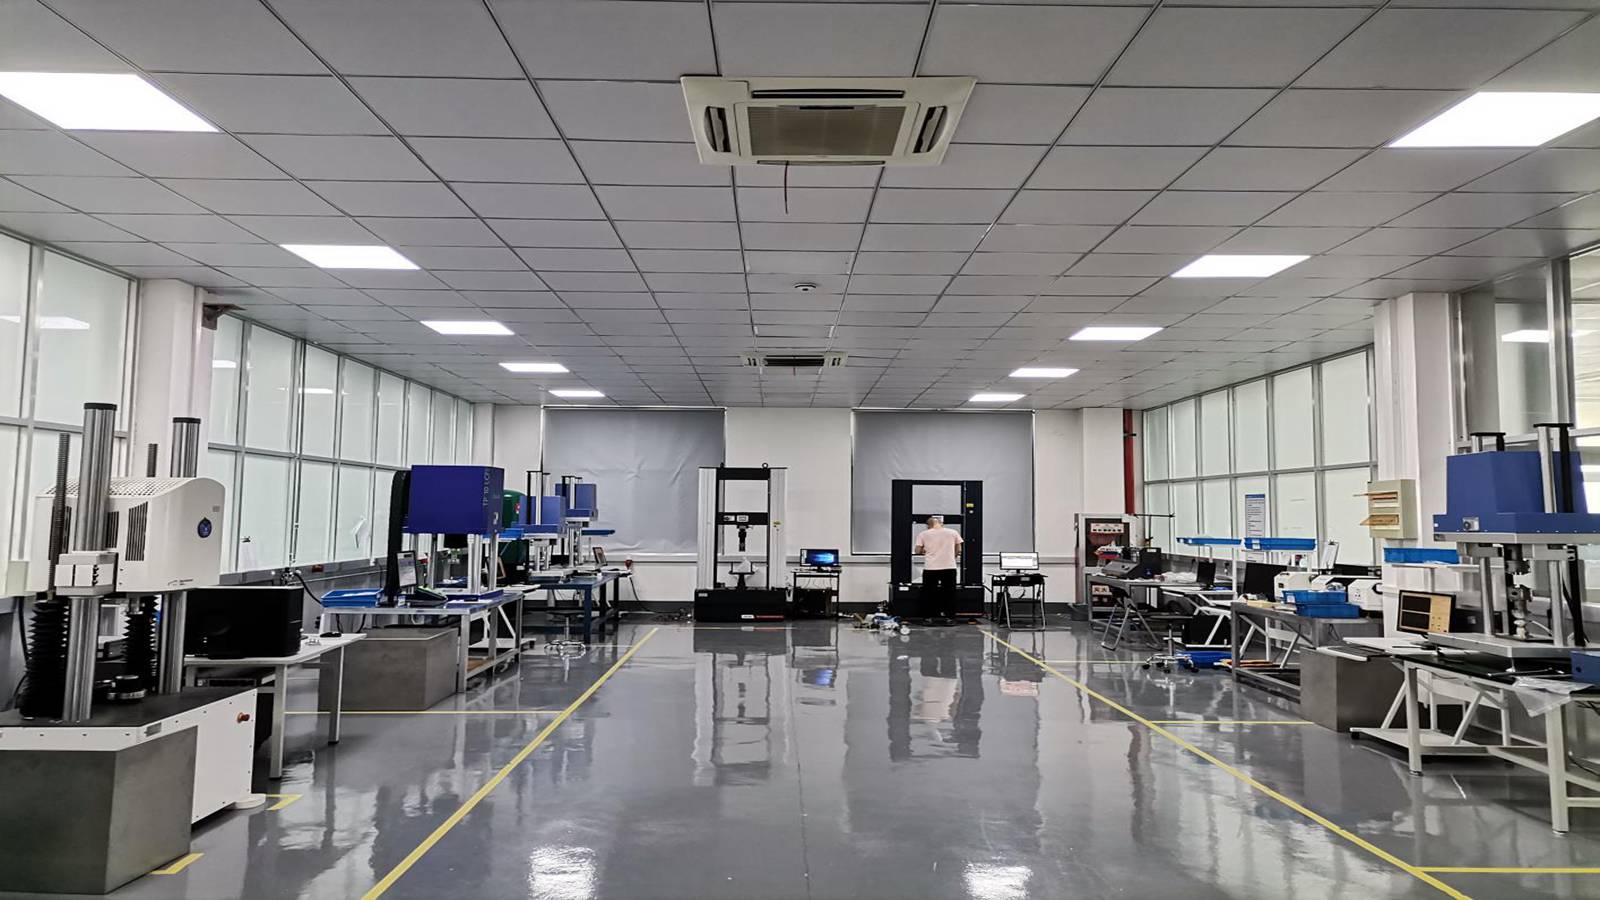
Founded with a commitment to human health engineering, HBM Medical Apparatus And Instruments Co., Ltd. operates a state-of-the-art manufacturing facility spanning over 30,343 square meters. Equipped with more than 350 advanced processing and testing machines—including 5-axis DMG MORI CNC milling machines, Citizen Swiss-type lathes, and Sodick wire EDM units—HBM manufactures spinal implants, cervical plates, pedicle screw systems, and trauma sets with tolerances controlled within ±0.005mm.
| Parameter | HBM Factory Standard Capabilities | Clinical Benefit for Grenville Providers |
|---|---|---|
| Raw Material Traceability | 100% Medical Grade Titanium (Ti-6Al-4V ELI) & PEEK (VESTAKEEP/Optima) | Zero risk of fatigue breakage; total biocompatibility certification for long-term implantation. |
| Quality Inspectors | 36 Full-time QA/QC Specialists across 12 Automated Lines | Eliminates batch defects through 100% optical CMM dimensional inspection. |
| Global Regulatory Audits | MDSAP (C730178), CE MDR (EPT 0477.MDR), ISO 13485 | Smooth border clearance into Grenville and seamless hospital audit pass rates. |
| R&D Customization | 31 Engineers (1 Doctorate, 11 Post-Graduates) | Custom surgical tray design, bespoke tap threads, and ergonomic handle modification. |
Quantifiable operational excellence serving international orthopedic distributors and OEM brand partners.
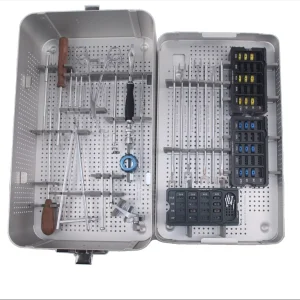
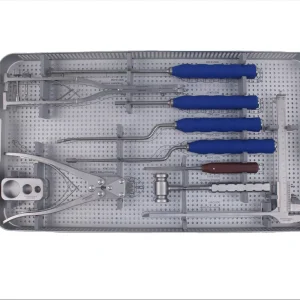
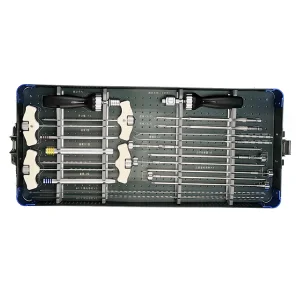
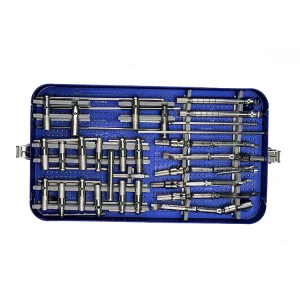
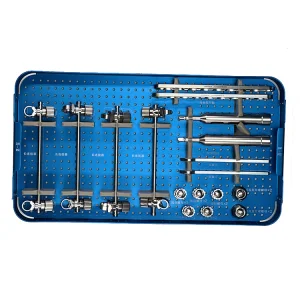
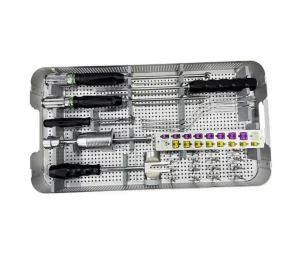
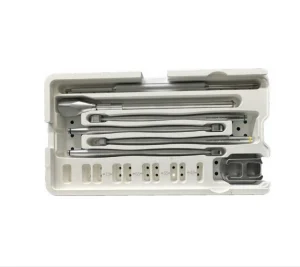
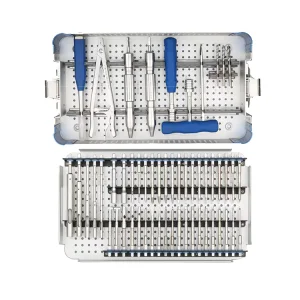
HBM Medical provides turnkey surgical tray configurations across major orthopedic and neurosurgical sub-specialties. Our instruments are surface-treated via hard anodization, electro-polishing, and micro-blasting to minimize glare under operating room luminaires and resist stain accumulation during washing cycle automation.
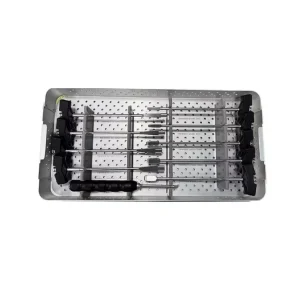
Includes 5.5mm/6.0mm/7.5mm polyaxial and monoaxial pedicle screw drivers, rod benders, distraction/compression forceps, and MIS percutaneous passage cannulas.
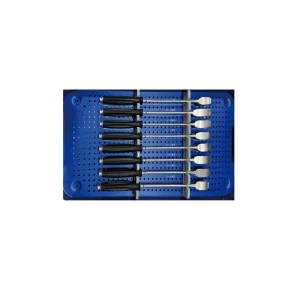
Complete cage inserters, trial rasps, sizers, and disc preparation instruments compatible with both radiolucent PEEK cages and 3D-printed Titanium lattice constructs.
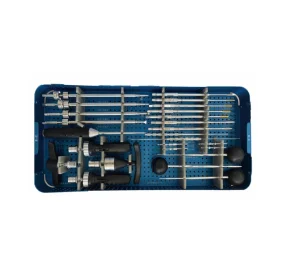
Broken screw removal instruments, universal hollow screw extractors, bone tap sets, and small-fragment locking plate instrumentation.
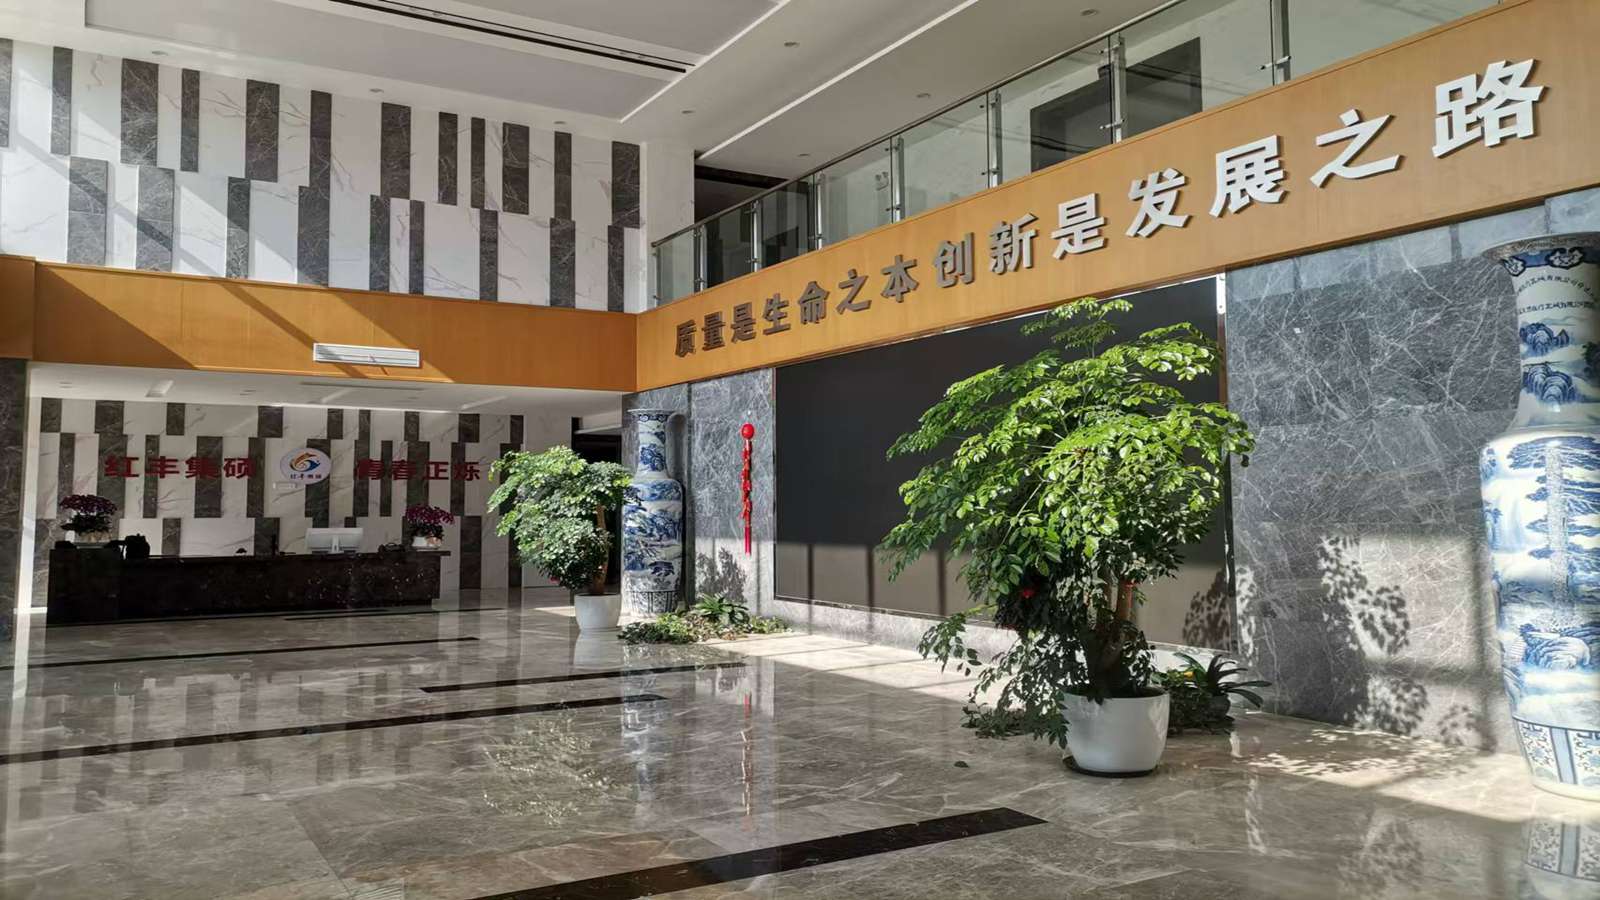
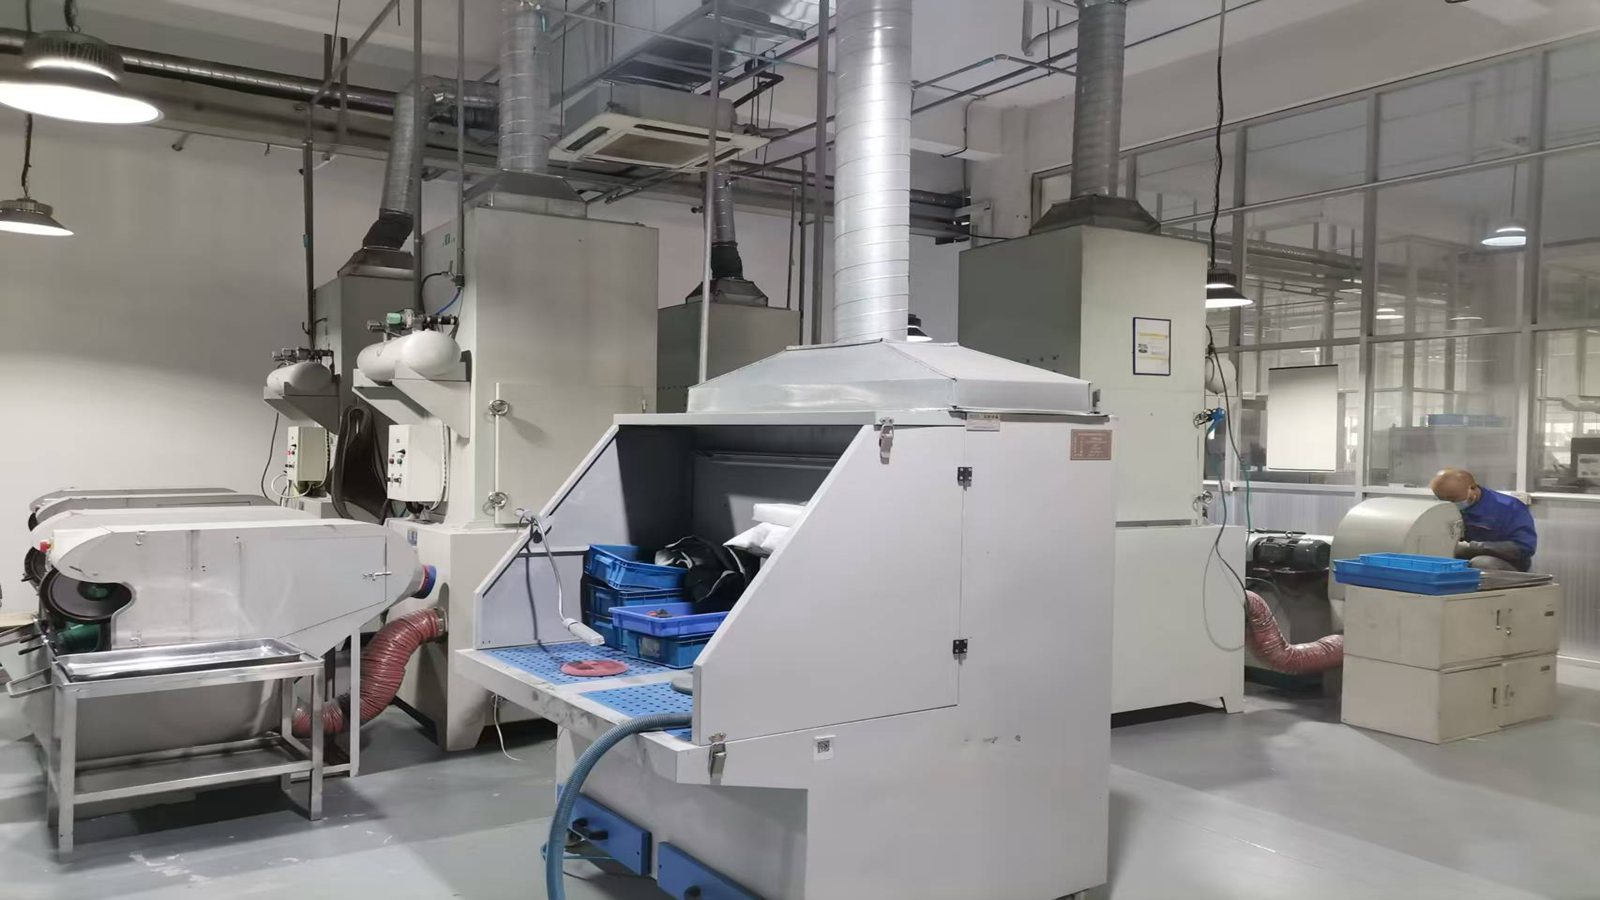
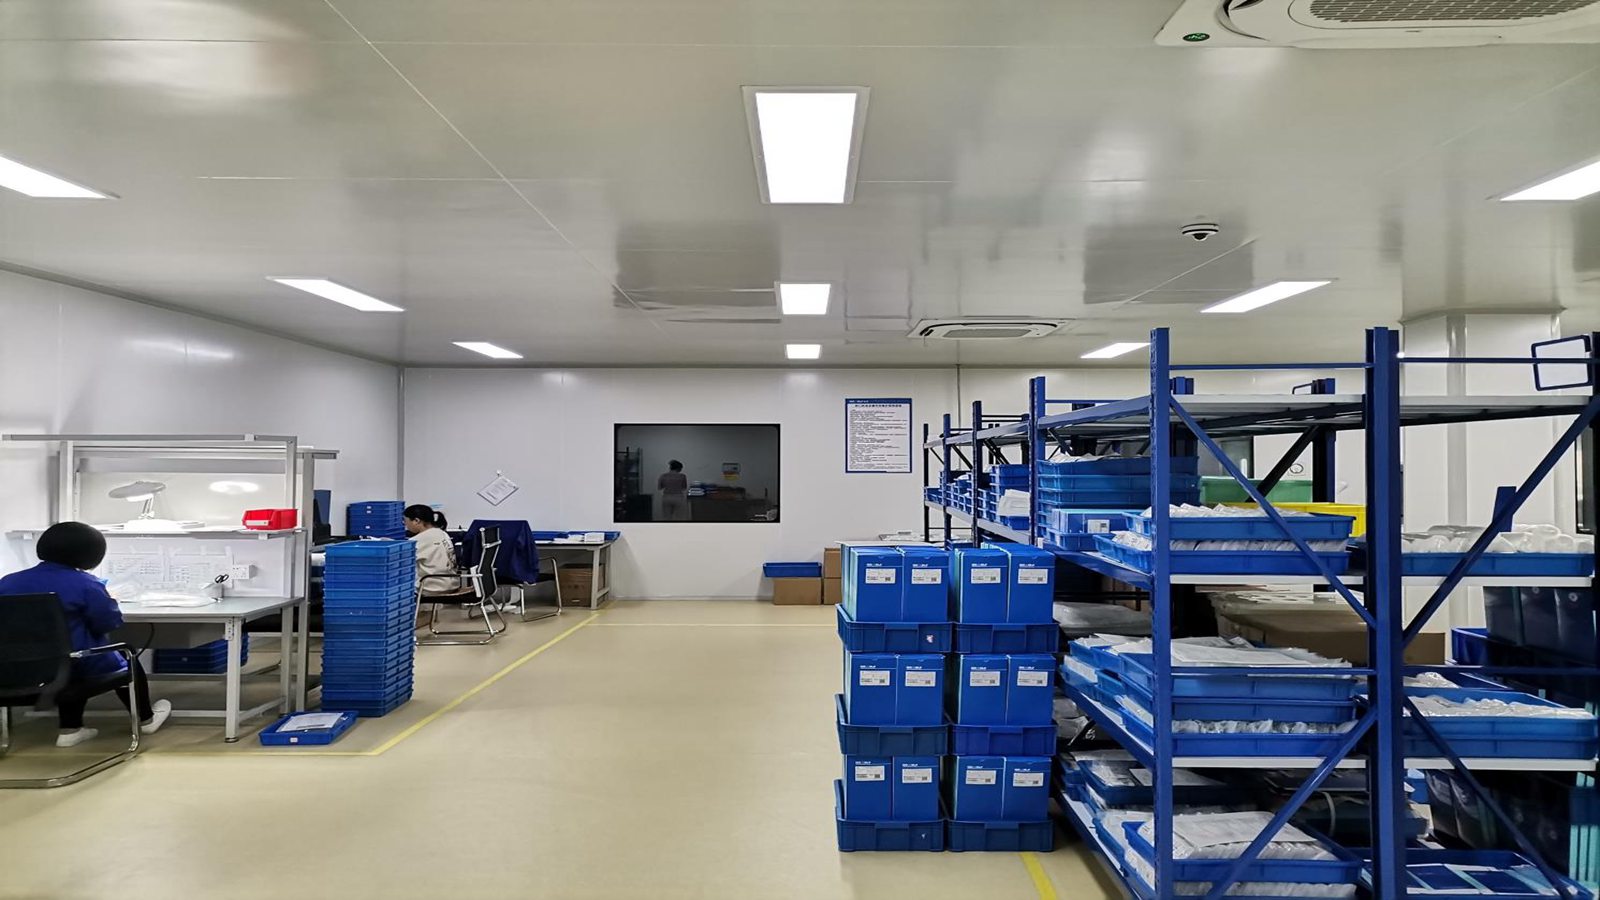
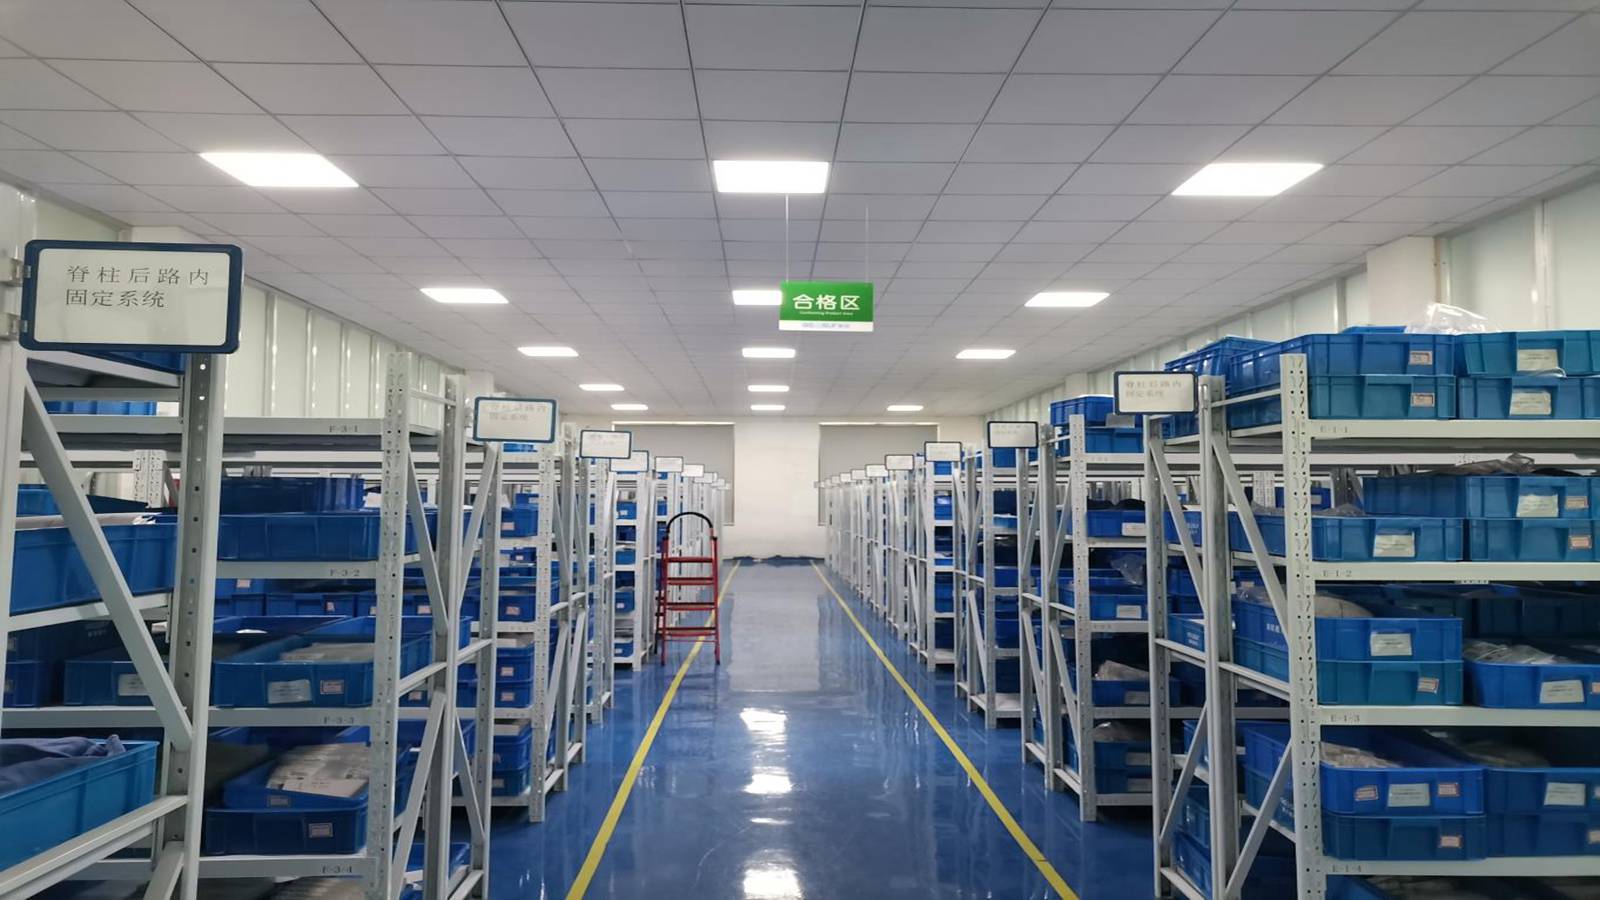
Inspect our ISO cleanrooms, 5-axis CNC machining bays, and certified quality laboratory.
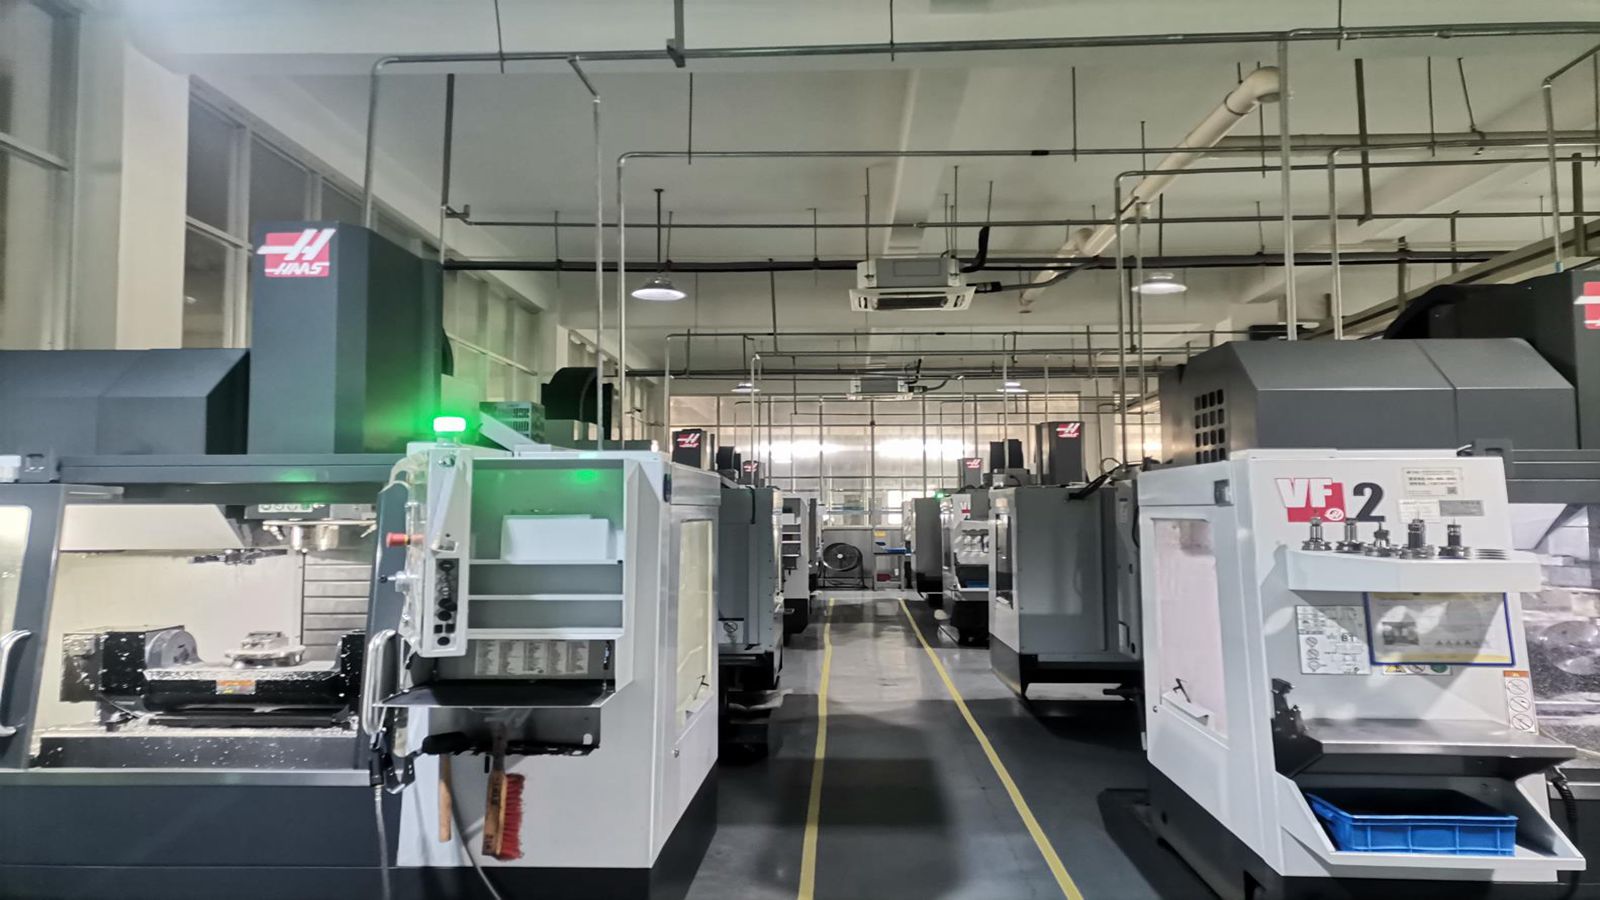
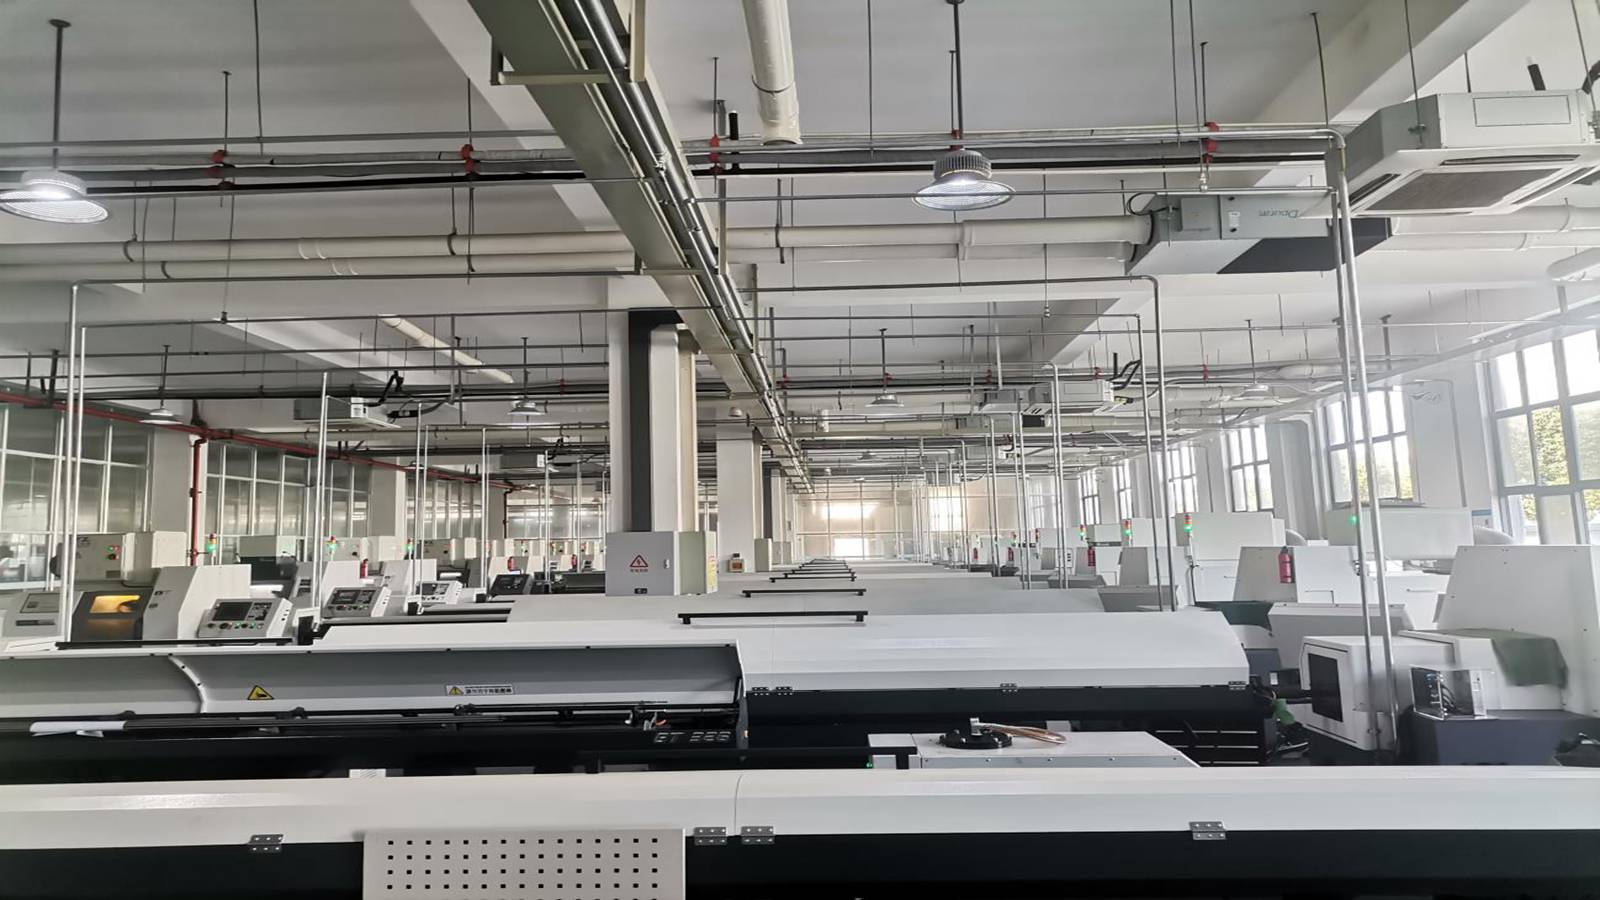
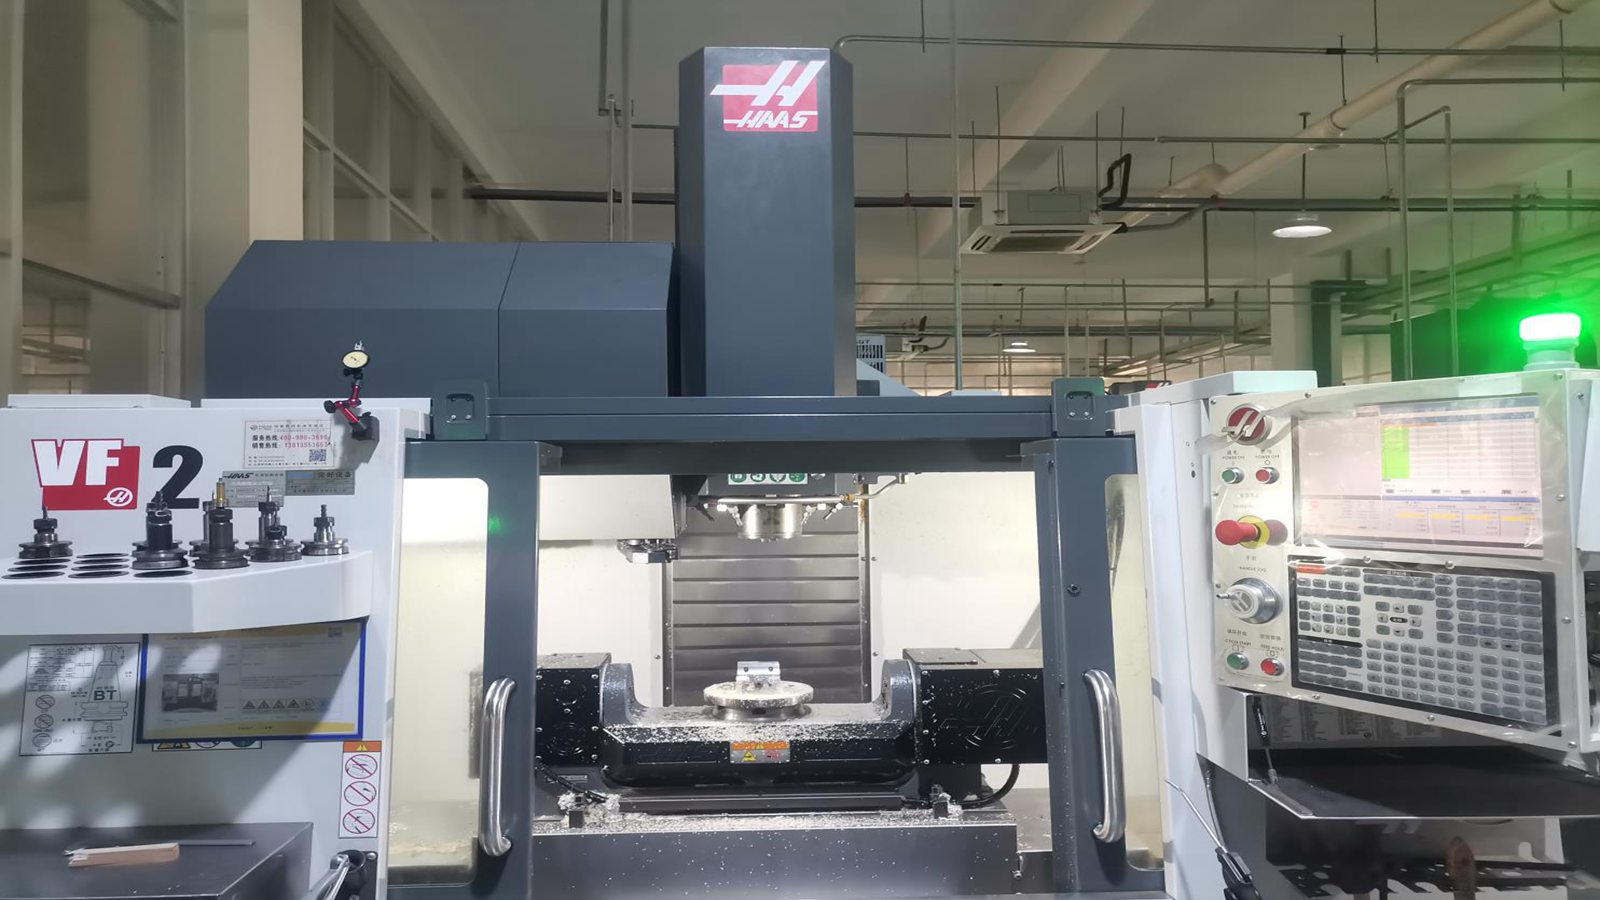
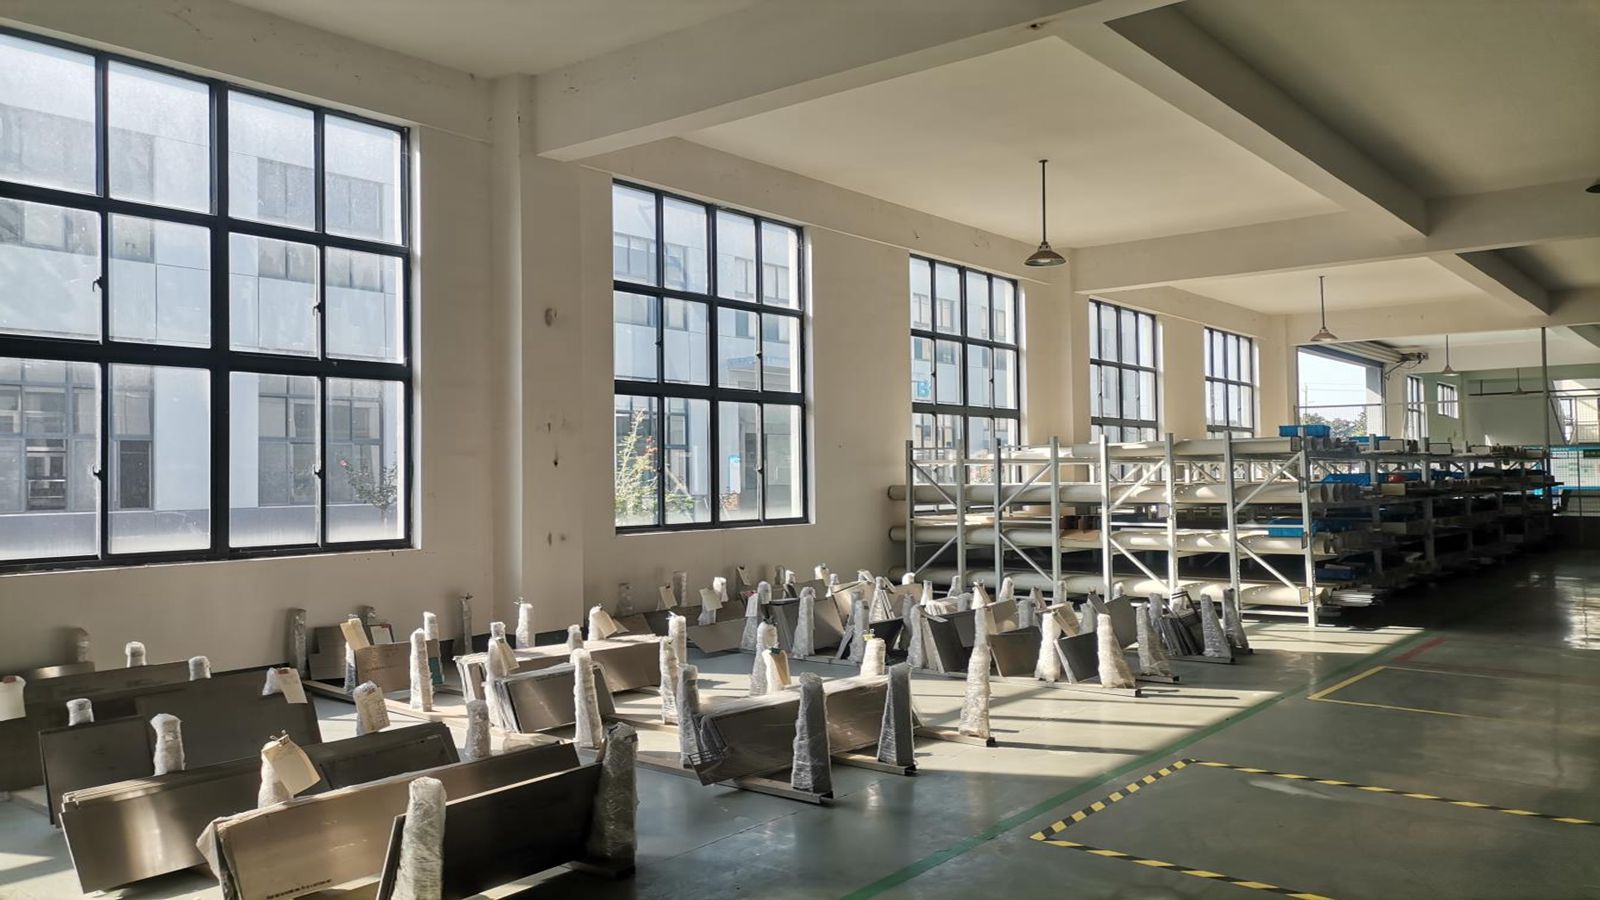
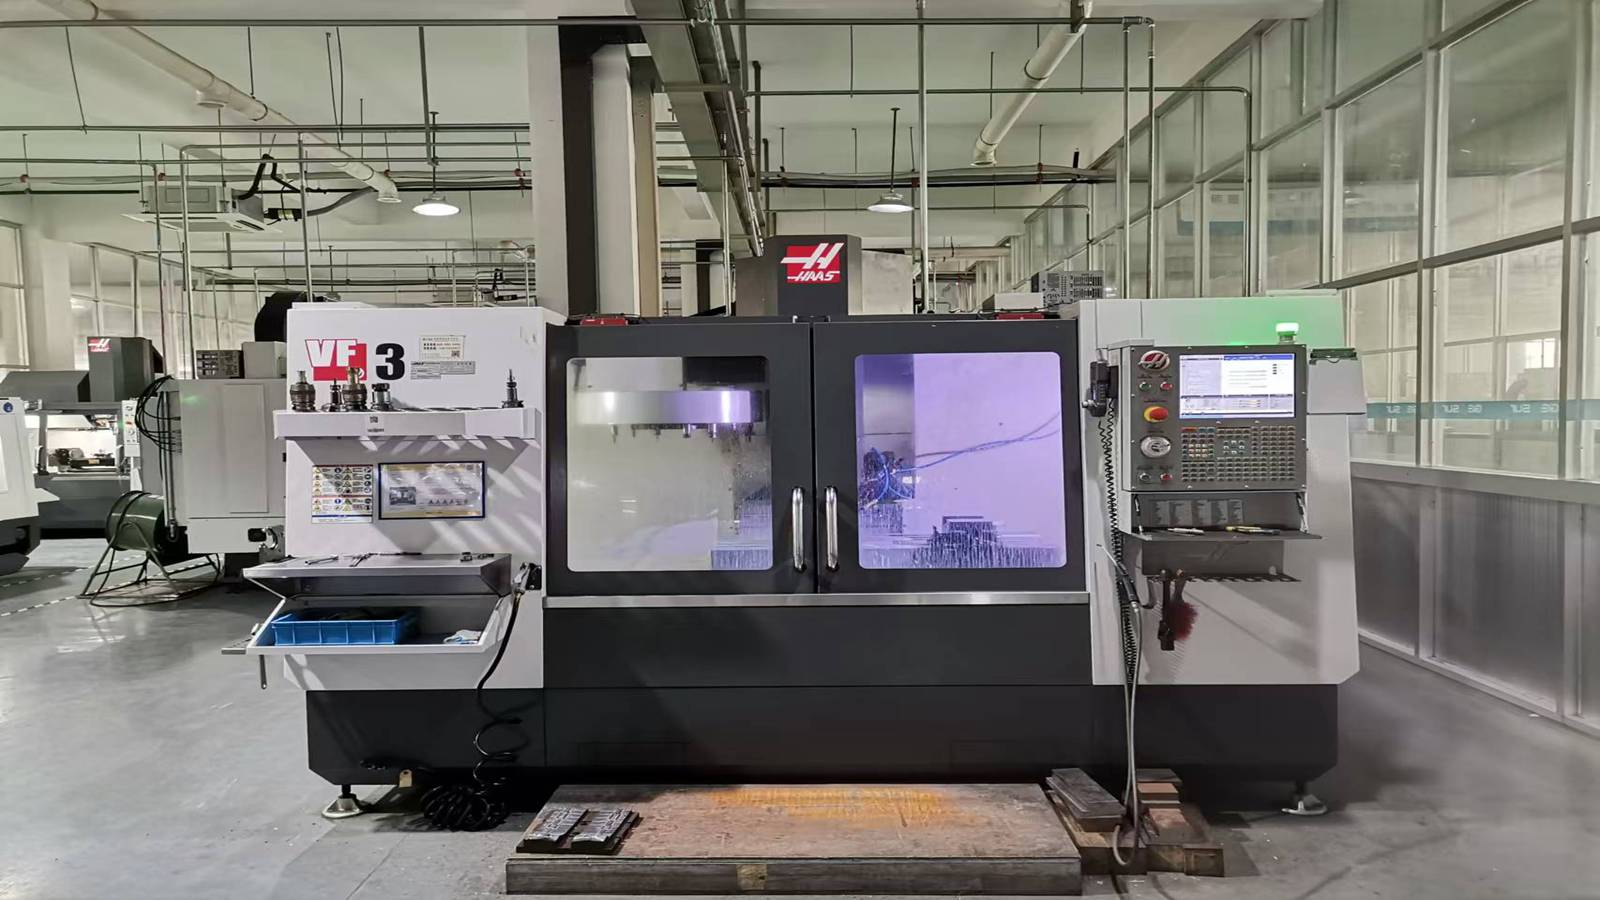
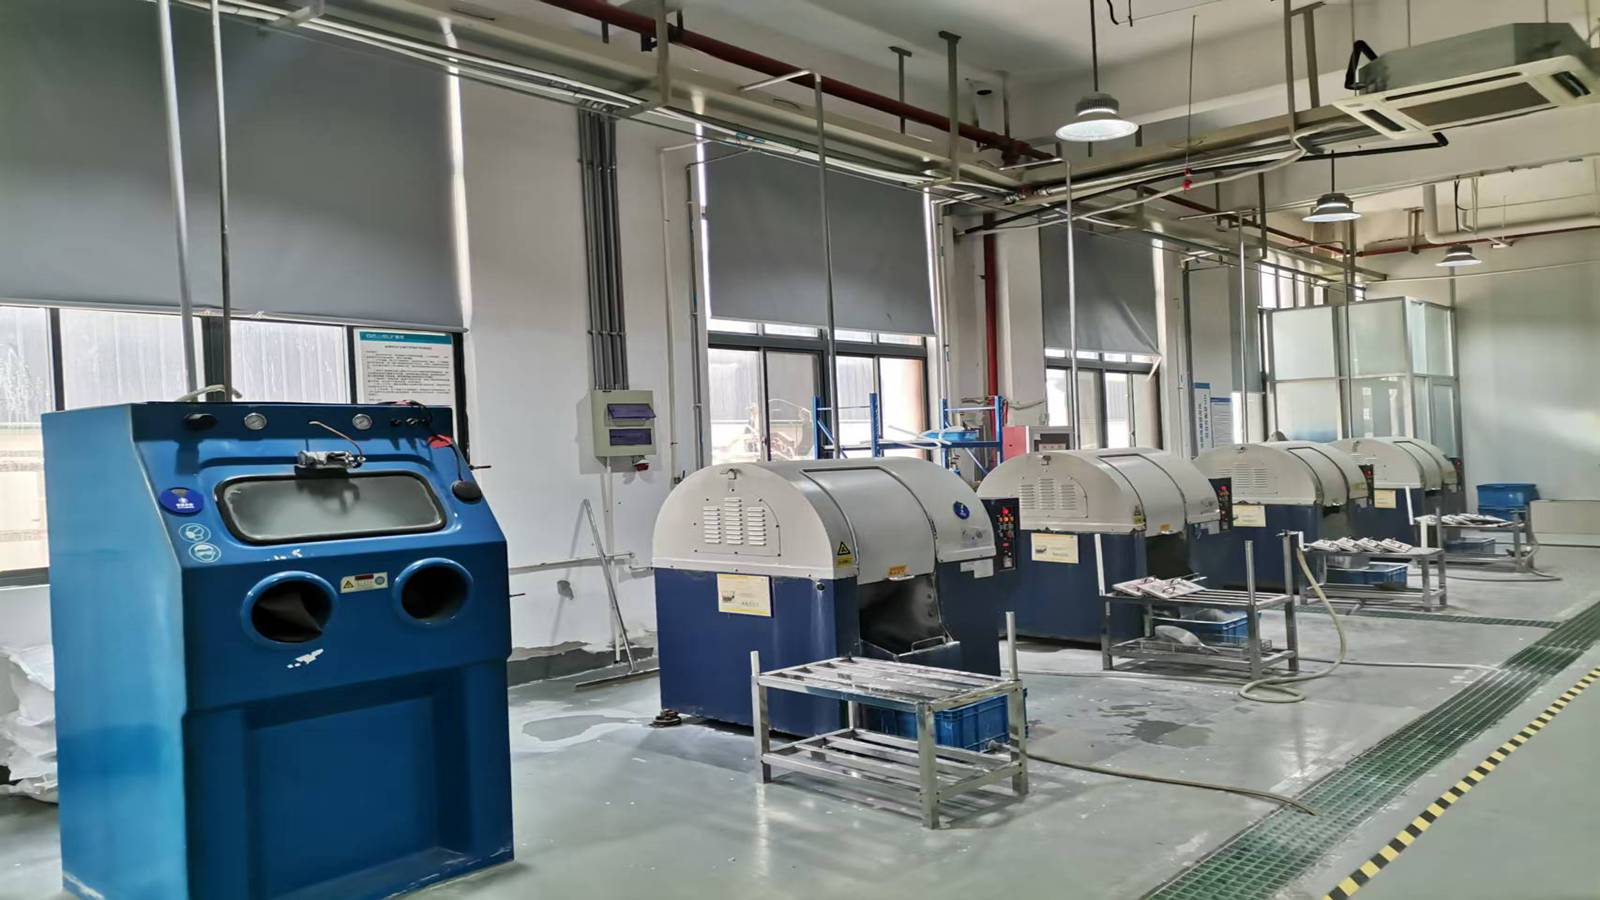
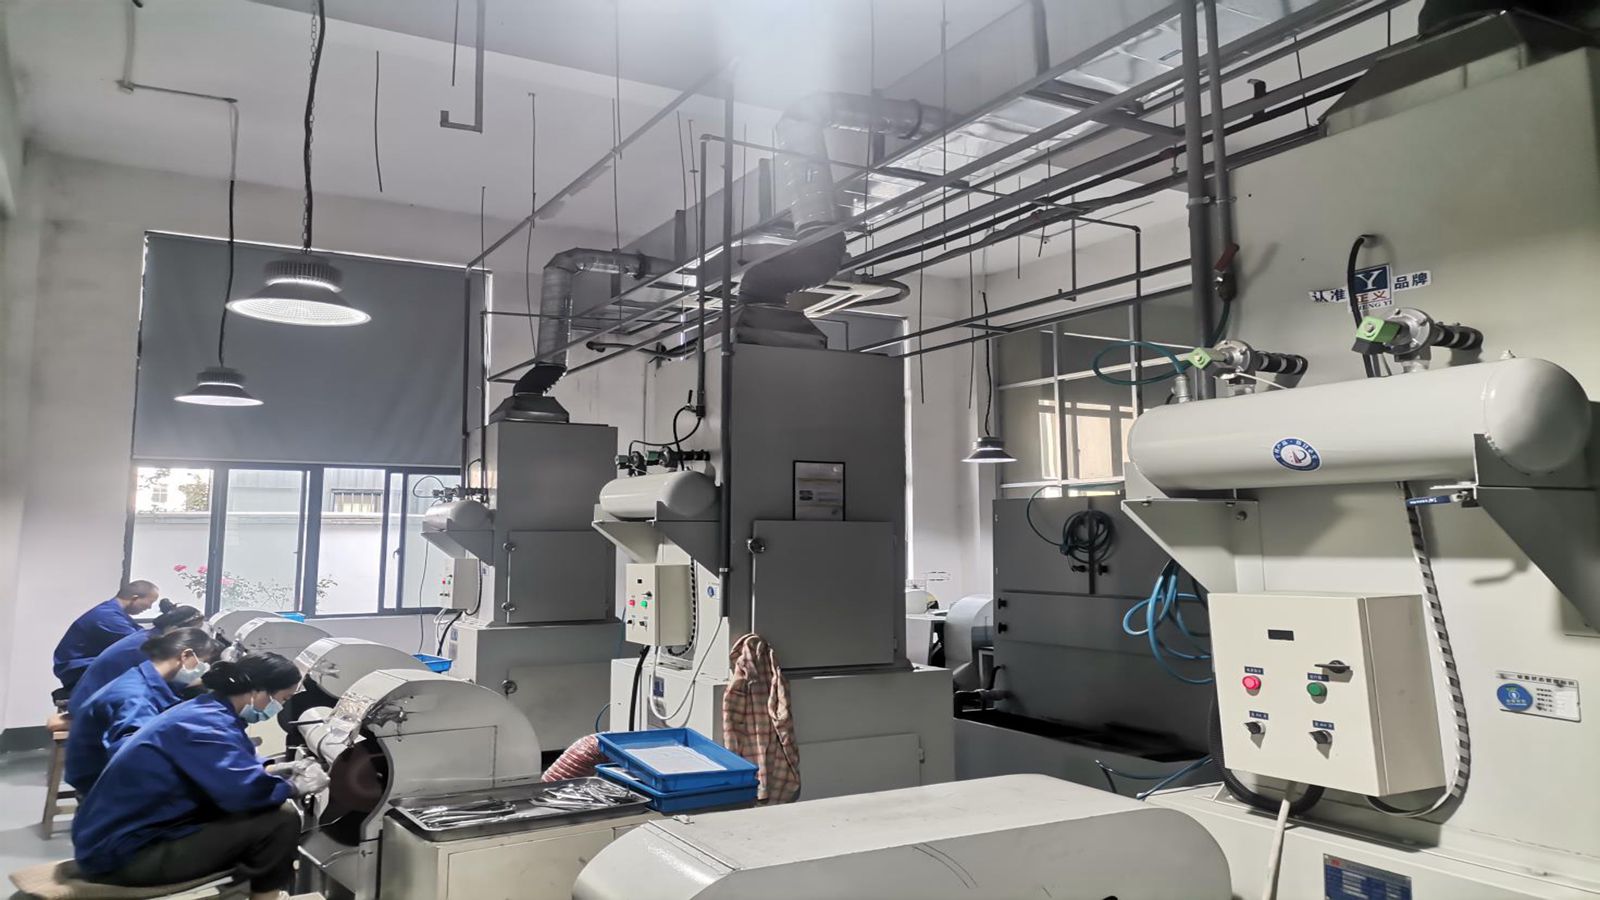
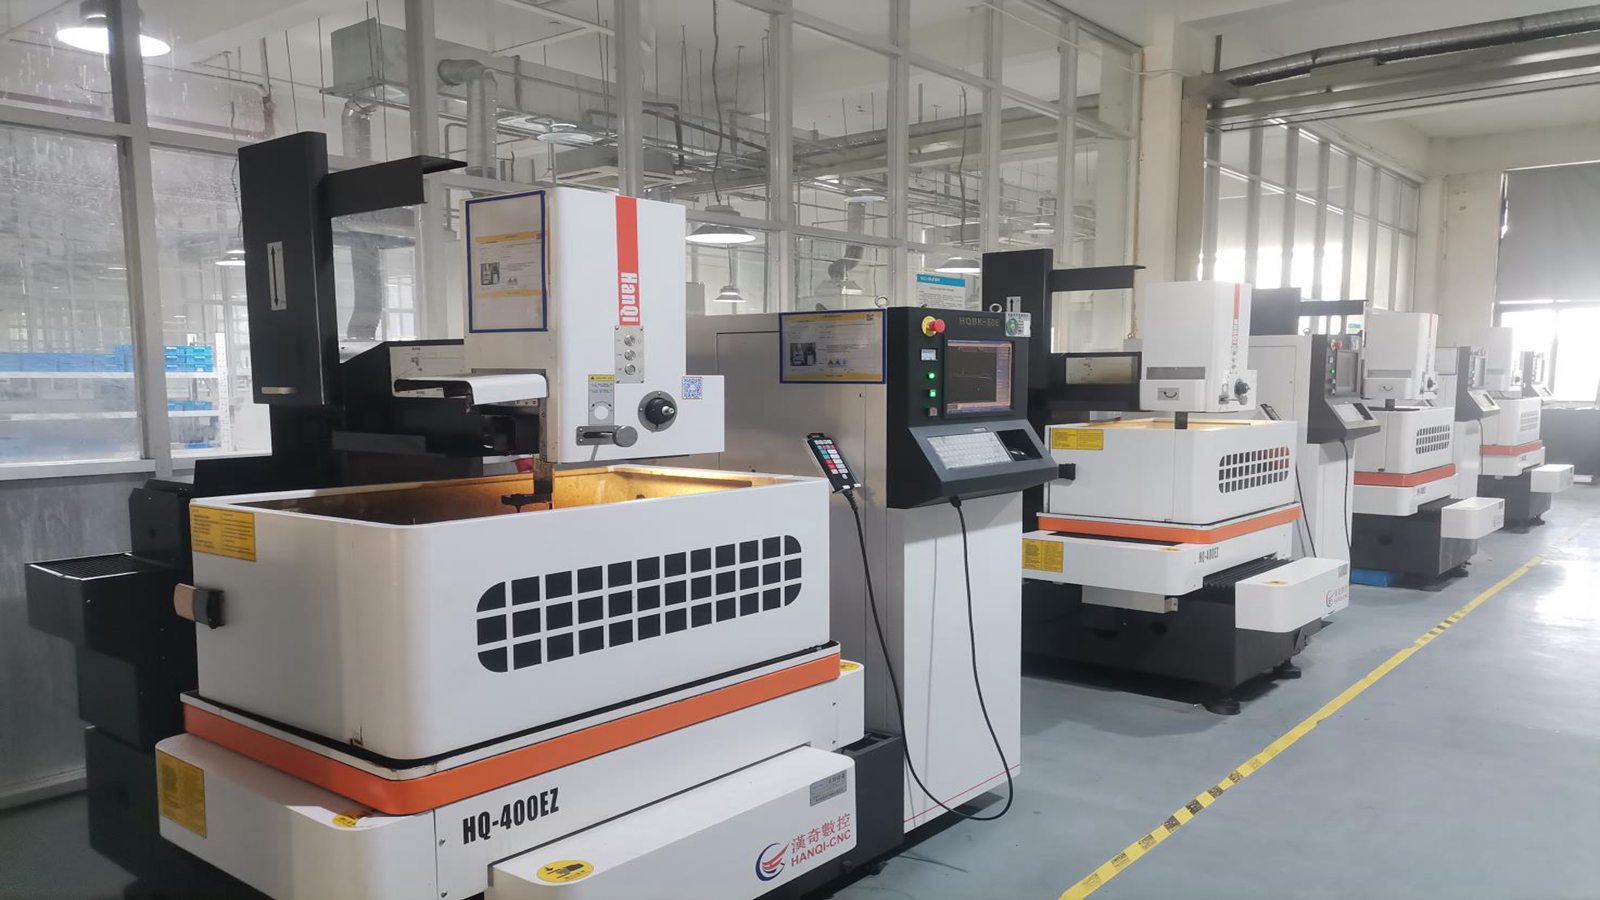
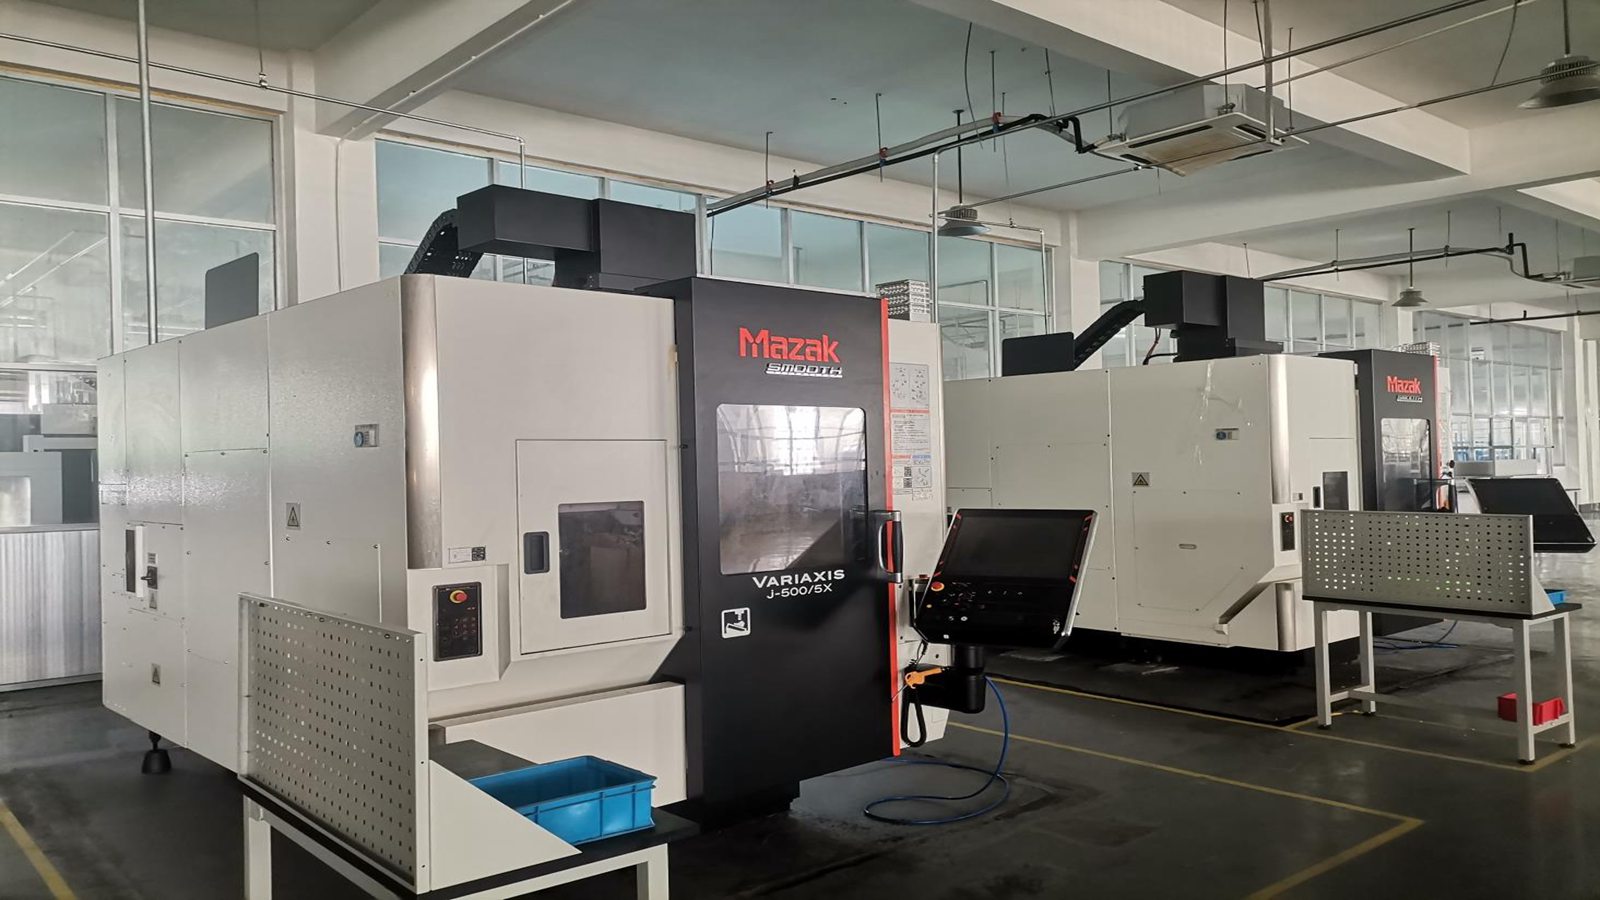
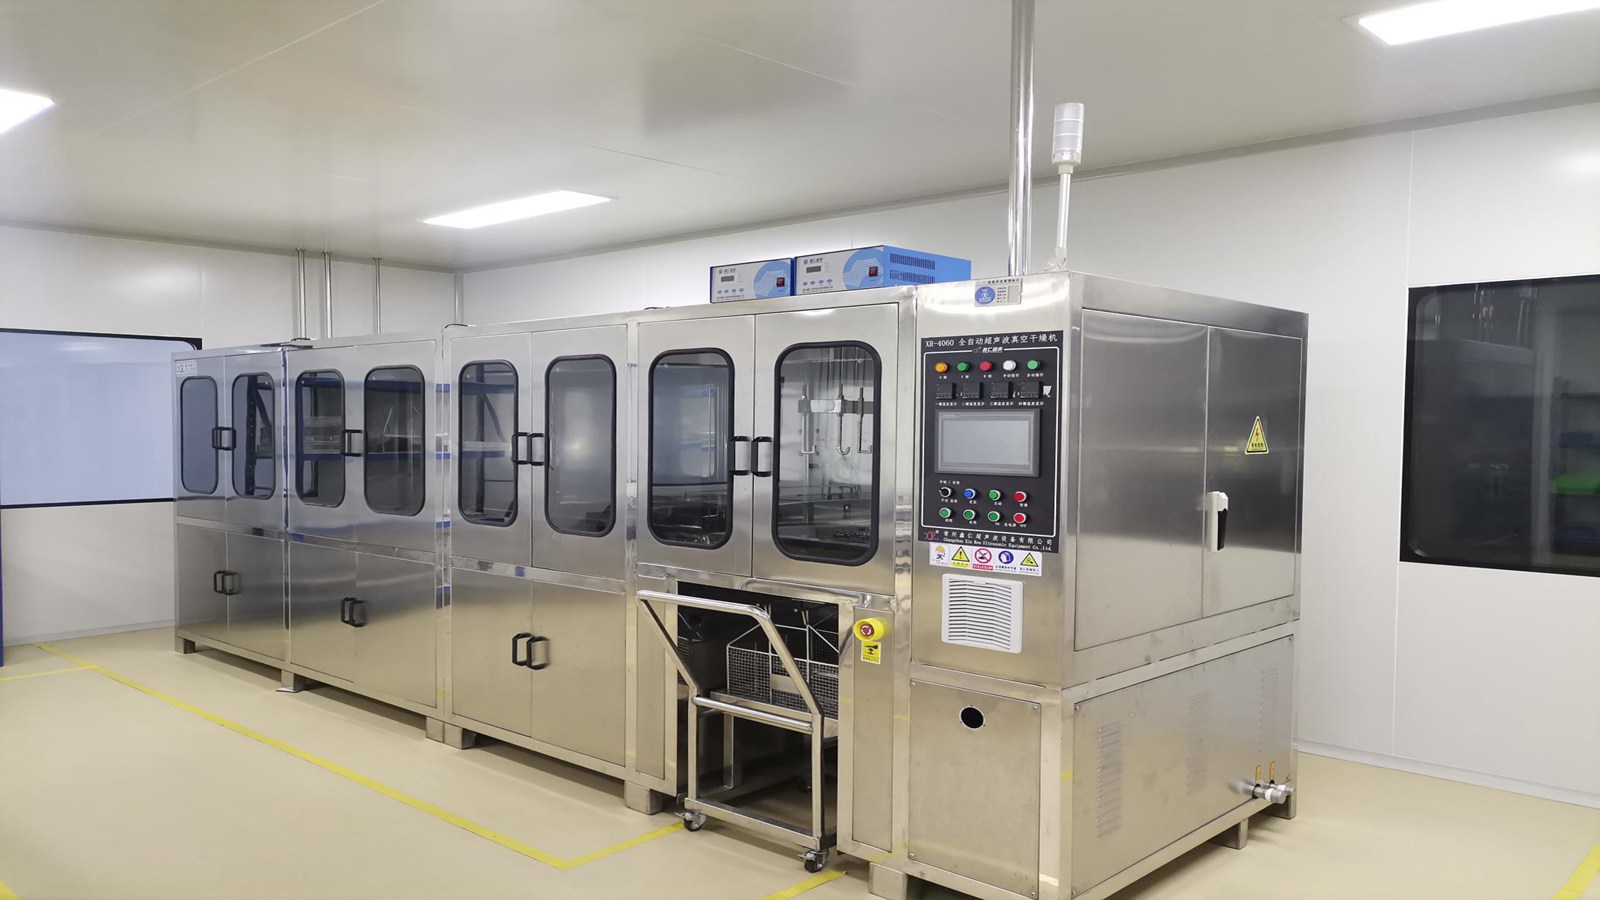
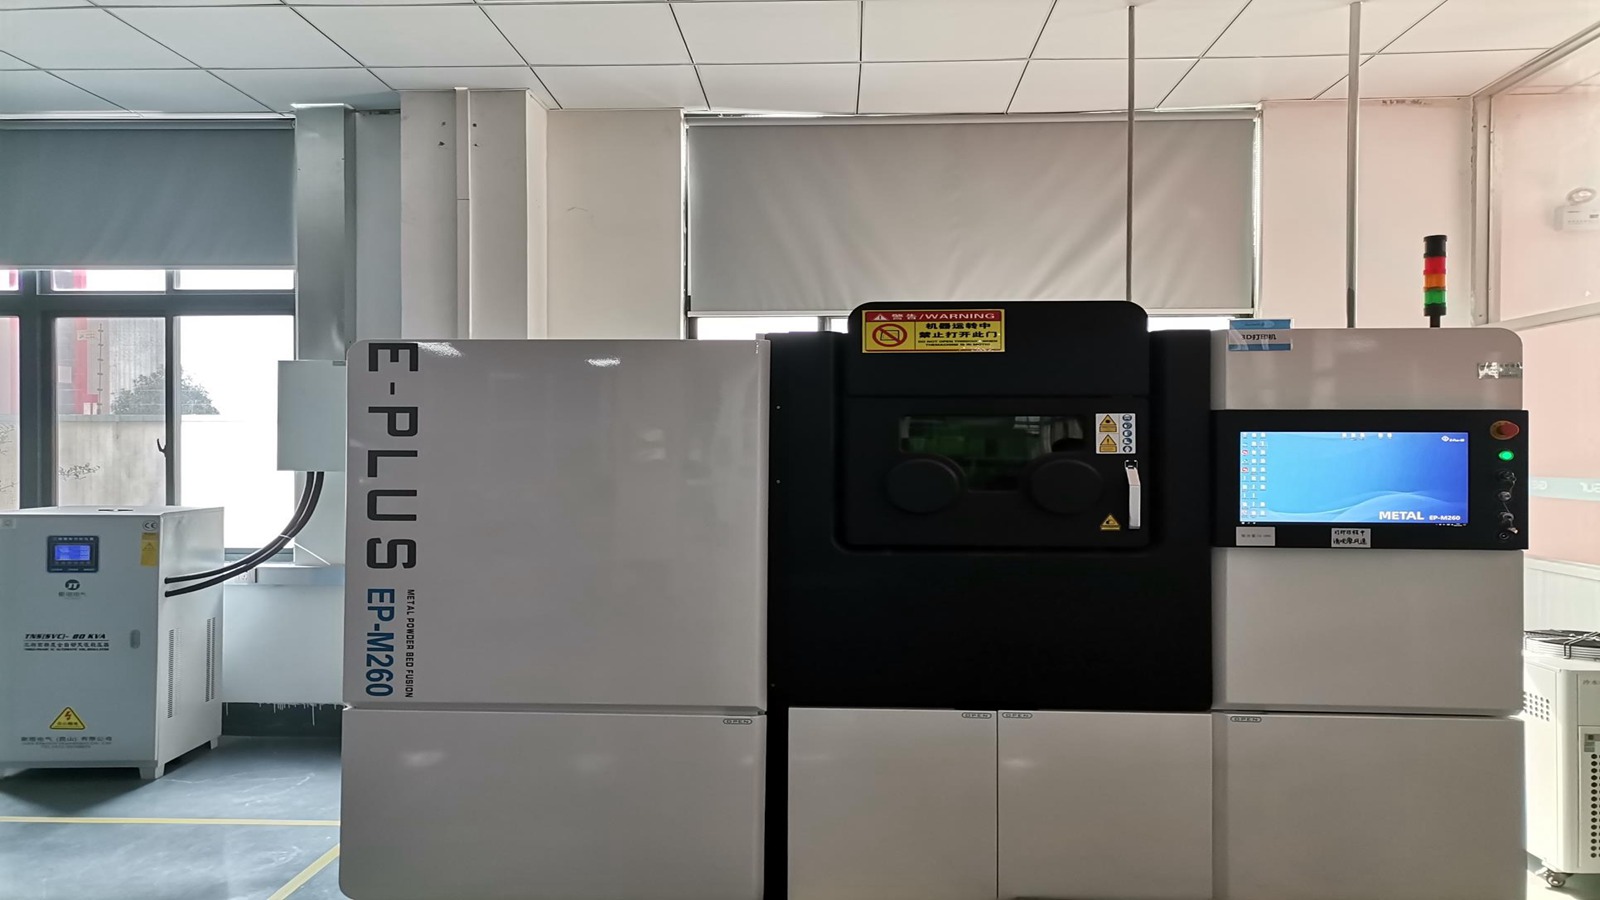
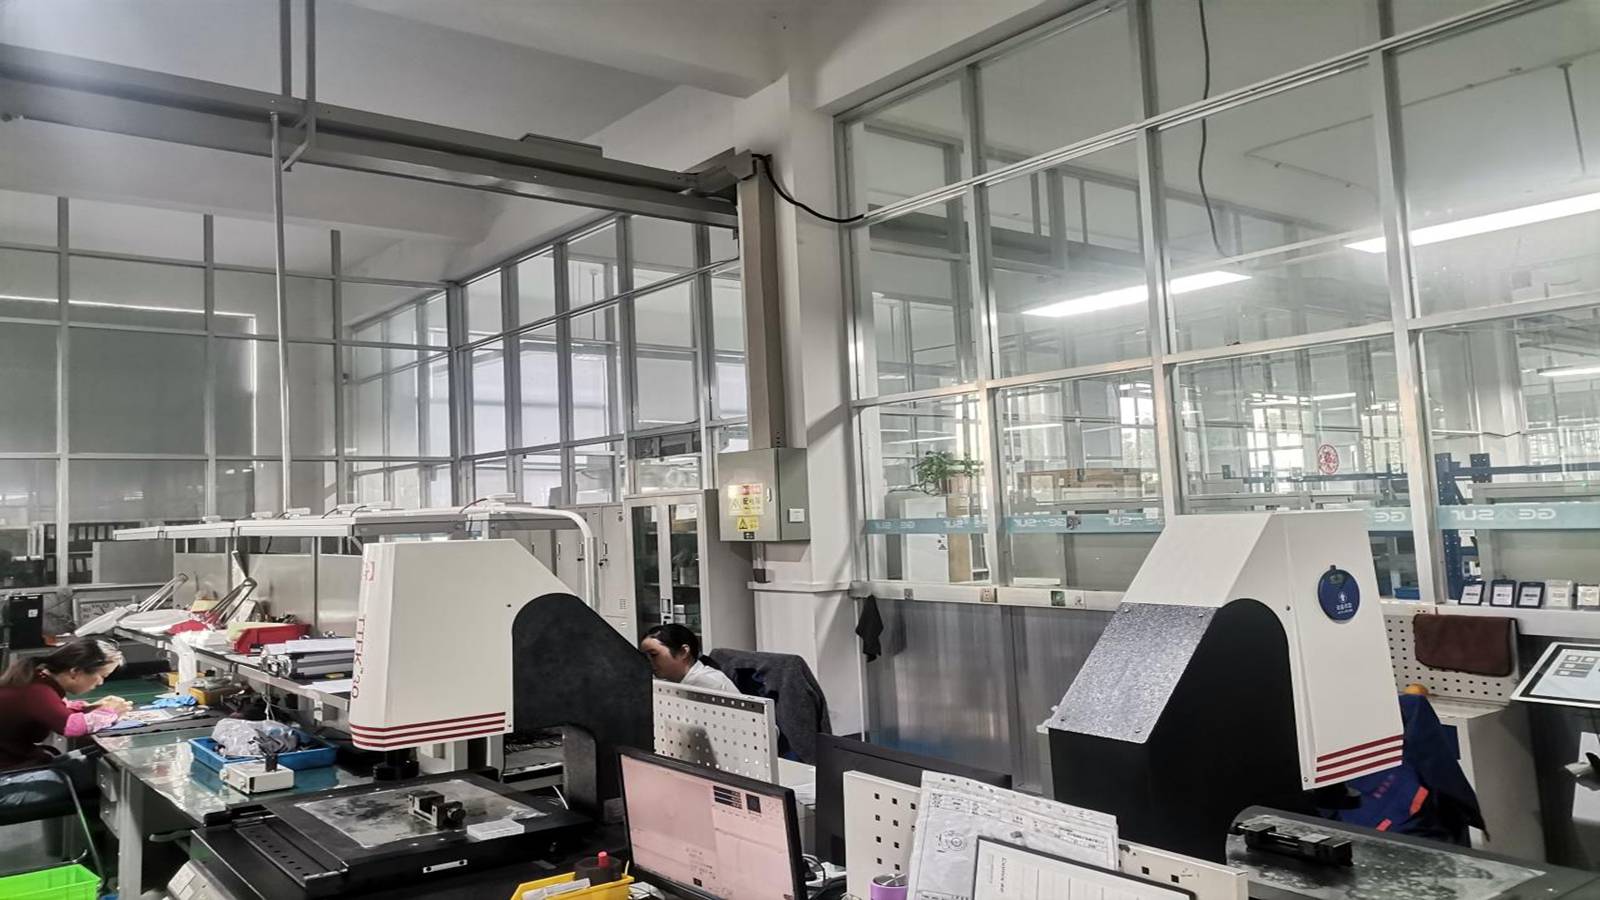
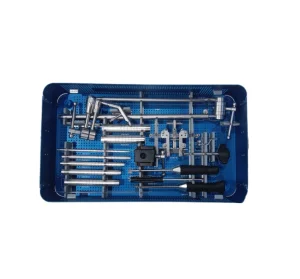
Explore our full line of cervical, thoracolumbar, trauma, and screw extraction systems shipped directly to Grenville partners.
Technical answers regarding custom manufacturing, international compliance, quality control, and shipping to Grenville.
HBM Medical delivers an optimal balance of elite engineering precision and cost structure. With over 30,000 square meters of production space, 12 production lines, 120+ CNC processing machines, and certifications under MDSAP, CE MDR, and ISO 13485, we supply Grenville distributors with identical or superior titanium grade performance compared to Western OEMs at a significantly lower unit cost.
We utilize exclusively raw implantable grade Titanium Grade 5 (Ti-6Al-4V ELI) and implant-grade PEEK (Polyether ether ketone) sourced with full chemical and mechanical traceability. All incoming materials undergo spectrographic analysis before reaching CNC production lines.
Yes. Our engineering team (comprising 31 R&D staff members with doctorate and master’s degrees) offers graphic customization, sample processing, and custom tray layout design. We can brand surgical handles, laser-etch custom sizing marks, and configure specialized instruments for MIS, OLIF, ALIF, or PLIF procedures.
Our facility employs 36 QA/QC inspectors across every phase of production. We execute 100% optical CMM dimensional checks, torque threshold validation, surface finish roughness testing (Ra < 0.4µm), and rigorous fatigue strength evaluations under cyclic loading.
Standard catalog orders are processed and dispatched within 7–14 business days. Custom OEM orders requiring specialized tooling typically ship within 30 to 45 days via expedited air freight directly to Grenville regional delivery hubs with full customs documentation included.
Empower your Grenville clinical network with high-precision spinal systems, cervical plates, PEEK cages, and trauma instrumentation. Contact our technical engineering team for instant quotes and CAD specifications.
Send Inquiry Now - Immediate Direct-Factory Response HBM Medical